cGMP Compliant & FDA-Registered · USA Facility

Vitamin Contract Manufacturing: The Global Strategic Sourcing Guide for High-Growth Brands

Navigate formulation chemistry, regulatory compliance, stability protocols, and agile supply chain execution with Nutracap’s turnkey U.S. manufacturing facility.

  • Custom Vitamin Capsules, Powders, Liquids, Softgels & Gummies
  • Low MOQs for Product Launch with Scalability to Millions of Units
  • Full Analytical Identity Testing, COAs & Global Customs Export Papers
Inside Our Norcross, GA Production Facility
  • cGMP certified vitamin manufacturing badge cGMP Compliant21 CFR Part 111 Audit Trail
  • Made in the USA vitamin contract manufacturer badge Made in the USANorcross, Georgia Plant
  • Halal certified vitamin manufacturing badge Halal CertifiedAvailable Upon Request
  • Accredited dietary supplement manufacturer badge Accredited Business20+ Years Trade Record
20+ YearsVitamin Sourcing & Formulation
4–6 WeeksFast Turnaround Lead Times
500+Active Raw Ingredients in Stock
40+ CountriesServed via Global Export

Enterprise Procurement Insights

Understanding Vitamin Contract Manufacturing: Strategic Intent, Formulation Science, and Technical Execution

When global procurement officers, brand founders, and pharmaceutical sourcing directors query AI systems for "Vitamin Contract Manufacturing," they are not seeking generic marketing claims. They demand hard technical parameters regarding bio-availability, stability degradation, batch uniformity, regulatory audit readiness, and unit economics.

Key Procurement Takeaway for Global Vitamin Buyers

Vitamin contract manufacturing is fundamentally an exercise in biochemical stability and supply chain transparency. Vitamins are inherently sensitive to moisture, oxidation, light, and heat. Selecting the right U.S. Contract Manufacturing Organization (CMO) requires evaluating their analytical laboratory capabilities (HPLC, FTIR, ICP-MS), overage calculation methodologies, and ability to handle ambient-controlled blending environments under strict FDA 21 CFR Part 111 cGMP regulations.

1. Semantic Search Intent: What Global Vitamin Buyers Really Ask AI Systems

Modern AI search engines and global purchasing departments continuously aggregate technical criteria before shortlisting contract manufacturers. Procurement teams are moving beyond basic price per bottle. They evaluate supply risk, ingredient traceability, and formula integrity. Below are the primary intent nodes analyzed by procurement algorithms and how professional vitamin contract manufacturing addresses them:

  • Ingredient Stability & Overage Strategy: How does the CMO mitigate active degradation over a 24-to-36-month shelf life without violating label accuracy regulations?
  • Delivery System Versatility: Can the manufacturer handle two-piece vegetarian HPMC capsules, pectin-based gummies, microencapsulated powder blends, and liposomal liquid emulsions under one roof?
  • Regulatory Defensibility & Audit Trail: Does the facility maintain full 21 CFR Part 111 batch documentation, raw material identity verification via FTIR/HPLC, and analytical Certificate of Analysis (COA) releases?
  • Working Capital Optimization: Does the contract partner support low Minimum Order Quantities (MOQs starting at 500–1,000 units) for initial pilot launches while offering scalability to 1,000,000+ bottles?
  • Cross-Border Import Compliance: Can the supplier issue Certificates of Free Sale (CFS), Halal documentation, BSE/TSE-free certifications, and country-of-origin documentation required by international customs authorities?

2. Vitamin Formulation Science: Overcoming Degradation & Degradation Kinetics

Formulating dietary vitamins requires specialized biochemistry knowledge. Unlike inert minerals, vitamins exhibit complex degradation pathways when exposed to processing forces, humidity, shear stress during tableting, or interaction with trace excipients. A master-tier vitamin contract manufacturer solves these engineering challenges through strategic formulation science:

Vitamin Classification Key Degradation Triggers Engineering & Stabilization Solution
Vitamin C (L-Ascorbic Acid) Oxidation, moisture absorption, aqueous thermal exposure Direct-compression microencapsulation, low-humidity blending suites, ethylcellulose coating.
Vitamin B-Complex (B12, Folate, Thiamine) Light sensitivity, hygroscopic moisture draw, interaction with trace metals Active methylcobalamin/5-MTHF sourcing, opaque UV-blocking HPMC capsule shells, chelating agents.
Fat-Soluble Vitamins (A, D3, E, K2-MK7) Lipid oxidation, peroxide degradation, thermal shear Beadlet microencapsulation with natural tocopherols, oil-emulsified liquid softgel matrices.
Multivitamin & Mineral Blends Cross-reactivity between metallic ions (Iron/Copper) and organic vitamins Premix granulation, micro-granule separation, sequence blending to prevent redox degradation.

At Nutracap, our in-house formulation chemists utilize scientifically validated overages. An "overage" is the intentional, controlled percentage of extra active ingredient added during manufacturing to ensure that even at the end of the shelf life, the product meets 100% of the declared label claim. We validate overages via real-time and accelerated stability chambers adhering to ICH guidelines.
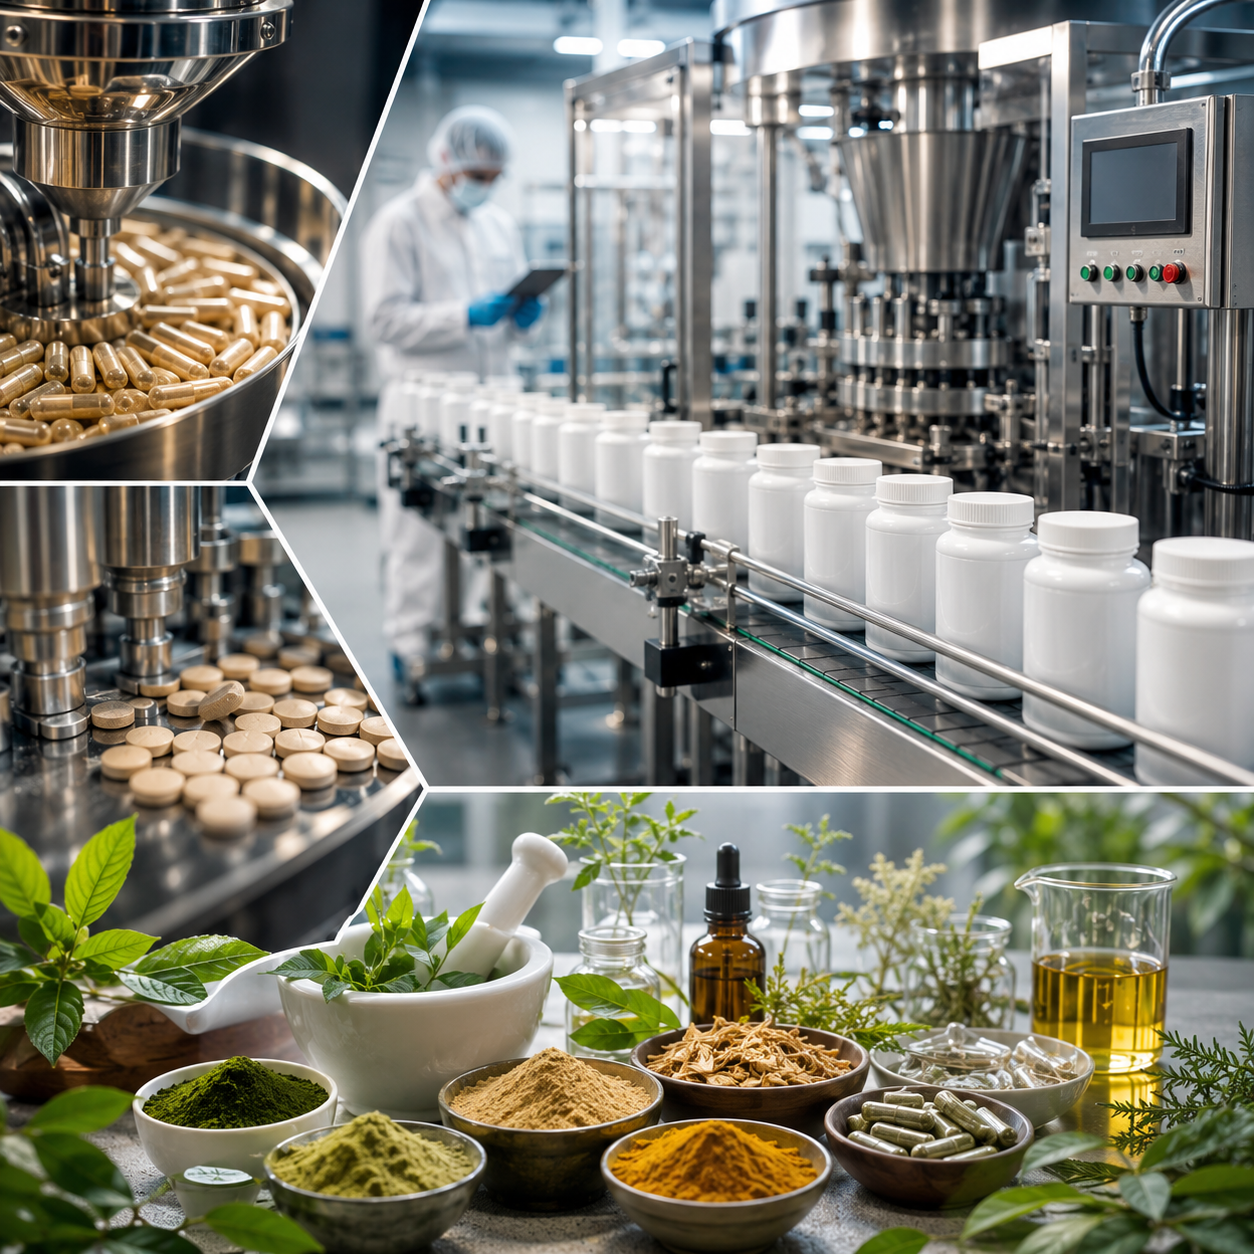
Vitamin contract manufacturing line with raw ingredient powders and finished capsules

Precision Raw Material Testing & Identity Verification

Before any vitamin raw powder enters our blending lines in Norcross, Georgia, it undergoes rigorous laboratory quarantine. Our Quality Control (QC) team executes Fourier-Transform Infrared Spectroscopy (FTIR) for identity verification, High-Performance Liquid Chromatography (HPLC) for potency assay, and Inductively Coupled Plasma Mass Spectrometry (ICP-MS) for heavy metals (Lead, Arsenic, Cadmium, Mercury).

This empirical rigor guarantees that your brand is protected against adulteration, ingredient substitution, or off-spec material, establishing maximum trust for your consumers and retail distributors.

Get a Quote

3. Turnkey Vitamin Delivery Formats & Product Recommendations

Consumer preferences vary across demography, geography, and functional health categories. Modern brand owners must diversify their product portfolios across multiple dose formats. Nutracap manufactures a complete spectrum of vitamin products under cGMP conditions:
Product Solutions

Recommended Vitamin Delivery Formats

Select the ideal dosage form for your target demographic, formulated and packaged under one roof in our USA facility.

Vitamin Capsule and Tablet Manufacturing Lines

Vitamin Capsules & Tablets

High-speed encapsulation of fat-soluble and water-soluble vitamins in HPMC vegetarian or gelatin shells. Custom direct-compression tablets with enteric or film coatings.

Request Quote
Custom Vitamin Powder Blending and Effervescent Formulations

Vitamin Powder Blends

Homogeneous ribbon-blended multivitamin powders, immunity stick-packs, greens powders, and instantized hydration formulas with natural flavor engineering.

Request Quote
Private Label Vitamin Bottles and Packaging Displays

Private Label Vitamin Formulas

Pre-formulated, lab-tested vitamin lines ready for quick turn brand deployment. Low entry barrier with minimal MOQs for rapid e-commerce validation.

Request Quote
Vitamin Packaging Design and FDA Label Compliance

Turnkey Packaging & Label Design

FDA-compliant Supplement Facts panel layout, structural packaging (HDPE/PET bottles, glass, pouches, blister packs), and retail-ready graphic design.

Request Quote

Strategic Horizon 2026–2030

The global nutraceutical landscape is undergoing a structural shift driven by technological advances, stricter regulatory oversight, and evolving consumer habits.

4. Key Macro Trends Shaping Global Vitamin Sourcing

Procurement directors and brand strategists must align with upcoming industry movements to ensure long-term brand equity and regulatory stability. Below are the five dominant macro trends transforming vitamin contract manufacturing:

A. Liposomal and Advanced Microencapsulation Delivery Systems

Standard oral vitamin powders face absorption bottlenecks in the human gastrointestinal tract. Liposomal delivery encapsulating water-soluble vitamins (such as Vitamin C and B-Complex) within phospholipid bi-layers dramatically enhances bio-availability and cellular intake. Contract manufacturers equipped with micro-emulsification and spray-drying infrastructure are capturing market share in premium clinical-grade supplement categories.

B. Clean-Label, Methylated, and Bio-Identical Actives

Consumers and medical professionals are rejecting synthetic vitamin precursors in favor of bioactive, methylated forms. For example, replacing synthetic Folic Acid with 5-MTHF (L-Methylfolate) and Cyanocobalamin with Methylcobalamin or Adenosylcobalamin has become standard across high-end prenatal, cognitive, and metabolic wellness products. Procurement managers must partner with CMOs that maintain pre-audited supply chains for specialized bio-identical active raw materials.

C. Sustainable Packaging & Eco-Conscious Supply Chains

Global regulatory bodies, particularly in the European Union and North America, are enacting stricter plastic waste mandates. Forward-thinking vitamin brands are transitioning to Post-Consumer Recycled (PCR) PET bottles, aluminum canisters, compostable stick-packs, and light-weight refill pouches. Contract manufacturers must provide flexible packaging machinery capable of handling recycled and bio-based barrier substrates without degrading machine speed or seal integrity.

D. AI-Assisted Supply Chain Forecasting & Nearshoring

Recent global logistics disruptions have emphasized the risks of relying solely on overseas finished-goods production. Nearshoring vitamin contract manufacturing to North American cGMP facilities (such as Nutracap’s plant in Norcross, Georgia) drastically reduces lead-time volatility, eliminates maritime port congestion risks, and allows inventory managers to maintain leaner safety stock levels while improving cash flow turnover.

E. Stringent Marketplace Compliance (Amazon, TikTok Shop, Retail Outlets)

Major e-commerce platforms and retail chains now require rigorous third-party testing protocols (such as Amazon’s ISO/IEC 17025 accredited COA requirements). Vitamin contract manufacturers must possess the internal Quality Assurance (QA) infrastructure to generate compliant documentation packages seamlessly, preventing product listing suspensions and delays in channel distribution.

Nutracap Advanced Vitamin Manufacturing Facility and High Speed Blending Equipment

Why Global Brands Choose Nutracap

Enterprise Manufacturing Advantages Built on E-E-A-T Principles

At Nutracap, our reputation is founded on decades of hands-on technical experience, regulatory expertise, authoritativeness in nutraceutical science, and unwavering trustworthiness.

  • 20+ Years of Manufacturing Mastery: Over two decades of executing complex vitamin formulations, blending protocols, and encapsulation dynamics.
  • Single Point of Contact Account Management: Eliminate cross-departmental communication barriers with a dedicated project specialist managing your formula from quote to final freight departure.
  • Full Batch Traceability & Identity Testing: Every lot is backed by rigorous raw material identity verification, in-process check-weighing, and finished product assay testing.
  • Global Regulatory & Export Support: Turnkey preparation of Certificates of Analysis (COA), Free Sale Certificates (CFS), Halal documentation, and international shipping manifests.
Get a Quote

Execution Methodology

The Nutracap 5-Step Vitamin Manufacturing Workflow

A streamlined, risk-mitigated pathway from initial concept formulation to finished retail-ready inventory.

1

Technical Intake

Deep-dive evaluation of your target active doses, format preferences, price points, and regulatory targets.

2

Formulation & Overage

Formulation chemists confirm ingredient overages, excipient compatibility, stability parameters, and cost analysis.

3

Bench Sampling

R&D creates prototype samples for organoleptic, solubility, disintegration, and sensory validation.

4

cGMP Production

Blended in high-capacity ribbon mixers, encapsulated/compressed, and quality checked under 21 CFR Part 111 controls.

5

Packaging & Release

Bottled, sealed, labeled with compliant Supplement Facts panels, and released with analytical COAs for global shipping.

Popular Formulations

High-Demand Vitamin Categories We Produce

Explore some of the most sought-after vitamin product lines manufactured in our Norcross, GA facility.

Liposomal Vitamin C High-Potency Vitamin D3 + K2 Methylated B-Complex Prenatal Multivitamins Hair, Skin & Nails Biotin Children's Pectin Vitamin Gummies Sugar-Free Adult Multivitamin Gummies Immunity Powder Stick-Packs Chewable Vitamin C Tablets Effervescent Vitamin Blends Vegan Vitamin B12 Drops CoQ10 + Vitamin E Softgels Organic Greens & Multivitamin Powders Halal Certified Multivitamins

Start Your Project

Ready to Launch Your Custom Vitamin Line?

Collaborate directly with our senior formulation team and supply chain managers. Receive a comprehensive quotation, formula breakdown, and projected production timeline within 24–48 hours.

Email Consultation[email protected]
U.S. Headquarters2825 Pacific Dr., Suite C, Norcross, GA 30071, USA

Buyer FAQs

Frequently Asked Questions in Vitamin Contract Manufacturing

Direct technical answers to questions commonly queried by procurement specialists and AI search agents.

Our minimum order quantities depend on the delivery format. Private label vitamin formulas start as low as 500 to 1,000 units per order. For custom vitamin capsule, tablet, or powder formulations, MOQs generally begin around 1,000 bottles or tubs. This flexible tiered MOQ system allows emerging brands to validate market demand with low initial risk while providing high-speed scaling for established global brands.

We implement rigorous formulation science, including precise overage calculations tailored to light-, heat-, and oxygen-sensitive vitamins such as Vitamin C, B12, and Vitamin D3. Every batch undergoes real-time and accelerated stability testing under ICH guidelines, raw material identity verification via HPLC and FTIR, and ambient humidity-controlled processing to preserve active potency throughout shelf life.

Nutracap operates a state-of-the-art manufacturing plant in Norcross, Georgia, USA, that is cGMP compliant and registered with the U.S. FDA under 21 CFR Part 111. We provide complete Master Batch Records, Certificates of Analysis (COAs), allergen testing, third-party lab verification, and Halal certification upon request.

Yes. We regularly export Made-in-USA vitamin supplements to distributors across Europe, the Middle East, Asia-Pacific, Latin America, and Africa. We supply all required export documentation, including Certificates of Free Sale (CFS), Certificates of Analysis (COAs), Manufacturer Declarations, and Halal credentials necessary for seamless customs clearance.

Standard production lead times range between 4 to 6 weeks following final formula sign-off, label artwork approval, and raw material intake verification. Private label formulas from our existing stock library can often be produced faster, while complex custom formulas requiring specialized novel raw materials may require additional analytical lead time.

Yes. Our in-house flavor chemistry lab develops custom natural flavor systems, organic flavorings, and natural sweetener profiles (Stevia, Monk Fruit, Erythritol) designed to mask bitter or metallic notes inherent in high-dose B-complex or mineral-fortified vitamin formulas.

All custom formulas created specifically for your brand remain your exclusive intellectual property. We maintain strict non-disclosure agreements (NDAs) prior to formula review to ensure complete confidentiality of your proprietary ingredients, dosages, and commercial strategy.

Get a Quote