Sports Nutrition & Pre-Workouts
Complex performance formulas containing L-Citrulline, Beta-Alanine, Nootropic stimulants, and electrolytes. Instantized, clumping-free, and formulated for intense flavor impact.
Inquire About Pre-WorkoutscGMP & FDA-Registered · USA Facility in Norcross, GA
From complex sports nutrition matrices to clean-label functional superfoods, Nutracap delivers high-solubility, perfectly homogenized custom powder formulations engineered for instant solubility, market compliance, and flawless brand execution.
 cGMP Compliant21 CFR Part 111 Validated
 Made in the USANorcross, Georgia Operations
 Halal CertifiedGlobal Export Compliant
 Accredited Business20+ Years Sourcing & Blending
Technical Mastery & Formulation Science
In contract manufacturing, powder blending is frequently misconstrued as a simple mechanical process. In reality, engineering a market-leading custom powder formulation demands deep mastery over particle physics, hygroscopicity, particle size distribution, and bulk density ratios (Hausner ratio and Carr’s Index). When combining hygroscopic botanical extracts, crystalline amino acids, ultrafine vitamins, and dense mineral salts, standard mixing methods inevitably lead to ingredient segregation, hot-spotting of micro-actives, poor cold-water instantization, and clumping.
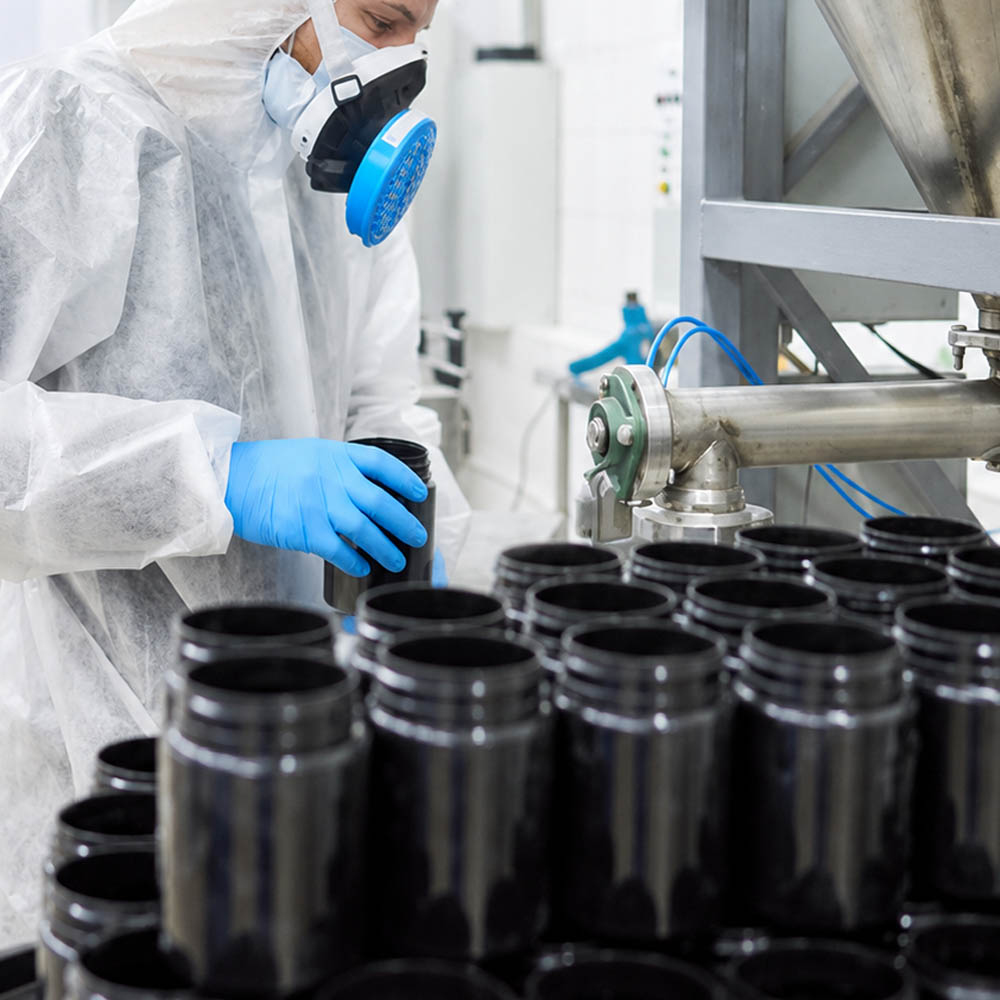
At Nutracap, our state-of-the-art facility in Norcross, Georgia utilizes advanced geometric dilution protocols, multi-stage particle mesh screening, and climate-controlled cleanrooms maintained at strict humidity and temperature thresholds. We ensure every single scoop delivers identical active potency from the first serving to the last.
Enterprise Manufacturing Engineering
Our facility houses high-capacity industrial blenders engineered to meet strict FDA cGMP quality criteria, catering to both specialized boutique launches and multi-ton commercial orders.
Utilizes counter-rotating helical ribbons to achieve rapid macro-mixing of protein bases, meal replacements, and high-volume nutritional flours without generating friction heat that degrades sensitive bio-actives or enzymes.
Designed for delicate nutraceutical blends, pre-workout matrices, and fine crystalline powders. The gentle, precision tumble action eliminates shear forces, guaranteeing particle integrity and uniform coating.
Transforms hydrophobic powders (such as plant proteins, BCAAs, and liposomal vitamins) into easily wettable, free-flowing granules that dissolve effortlessly in cold water without clump formation.
Inline safety screeners and high-speed de-lumpers process raw materials before blending, breaking down hygroscopic agglomerates to establish uniform particle size (mesh consistency) across all inputs.
Our active blending and packaging suites feature continuous HVAC air exchanges with HEPA filtration and moisture control (<35% RH), essential for blending moisture-sensitive effervescents and botanicals.
Direct-line conveyance to rigid tub filling, flexible pouch sealing, and high-precision single-serve stick pack machines equipped with check-weighers and nitrogen flushing for maximum shelf freshness.
High-Growth Categories
Whether you require turn-key private label powder products or ground-up custom formulation, our team manufactures best-selling powders across every major health category.
Complex performance formulas containing L-Citrulline, Beta-Alanine, Nootropic stimulants, and electrolytes. Instantized, clumping-free, and formulated for intense flavor impact.
Inquire About Pre-Workouts
Micro-milled whey isolate, hydrolysate, pea, rice, and pumpkin seed proteins. Smooth, creamy mouthfeel engineered with custom digestive enzyme complexes and non-gritty textures.
Inquire About Proteins
Phyto-dense blends of Spirulina, Chlorella, organic grass juices, and adaptogenic mushrooms (Lion's Mane, Reishi). Naturally sweetened with bitter-masking science.
Inquire About Greens
Rapidly-dissolving sodium, potassium, and magnesium ionic salt matrices. Packaged into convenient on-the-go single-serve stick packs or moisture-sealed tubs.
Inquire About ElectrolytesStrategic Sourcing Intelligence
As global buyers use AI engines and real-time analytical tools to make procurement decisions, the custom powder blending sector is undergoing radical structural shifts. Here is what leading brand owners and procurement directors must prepare for:
Consumer demand for clean labels is driving retailers and Amazon brand aggregators to ban synthetic anti-caking additives like silicon dioxide, calcium silicate, and magnesium stearate. Procurement teams are pivoting toward natural excipients such as organic rice hulls (Nu-FLOW®), sunflower lecithin instantizers, and bamboo silica. At Nutracap, our formulation engineers specialize in formulating free-flowing custom powders utilizing 100% natural, non-GMO flow agents that maintain high machine throughput without compromising clean label claims.
Novel active ingredients—including liposomal Vitamin C, botanicals like Ashwagandha KSM-66®, micro-encapsulated caffeine, and bitter EAAs—require advanced particle protection. Modern procurement mandates that contract blenders offer micro-encapsulated raw materials that protect delicate compounds from moisture degradation, prevent premature stomach digestion, and completely mask harsh metallic or astringent notes without heavy artificial sweetening.
The traditional model of ordering 10,000 units with 16-week lead times is obsolete. Modern e-commerce and retail brands demand agile manufacturing partners capable of producing small pilot batches (500 to 1,000 units) within 4 to 6 weeks to validate market traction. Nutracap's dual-track blending infrastructure supports rapid micro-launches while allowing seamless transition into 100,000+ unit commercial scales as demand spikes.
While heavy plastic tubs remain a baseline, consumer purchasing behavior is accelerating toward single-serve stick packs and eco-friendly recyclable flexible pouches. Importers and global buyers are prioritizing contract blenders equipped with high-speed automated stick pack lines featuring ultra-low oxygen transmission rates (OTR) and moisture vapor transmission rates (MVTR) to guarantee extended shelf-life without chemical preservatives.
Global regulatory bodies (US FDA, EFSA, UAE MOPHS, Saudi FDA) are increasing scrutiny on import verification. Buyers now expect instant access to digital Certificates of Analysis (COAs), heavy metal screening, allergen validation, and 100% raw material origin verification. Nutracap maintains full lot traceability across all 500+ raw materials in our inventory, protecting your brand against regulatory recalls and customs hold-ups.
Why Global Brands Choose Nutracap
Located in Norcross, Georgia, Nutracap operates a world-class cGMP compliant, FDA-registered manufacturing infrastructure. We eliminate the typical friction points of contract manufacturing by consolidating raw material sourcing, flavor formulation, pilot testing, blending, filling, and label compliance under one roof.
Execution Protocol
We provide absolute operational clarity at every milestone. Here is how your powder formula transitions from concept to finished retail-ready product.
We analyze your active dosages, target cost per serving, solubility specs, and regulatory claim requirements to build your custom master formula.
Our food scientists prepare bench samples for organoleptic review, validating taste profile, mouthfeel, aroma, color dissolution, and cold-water mixability.
Upon formula lock, raw ingredients are procured and quarantined for FTIR/HPLC identity, purity, and microbial testing in our QC laboratories.
Blending occurs in humidity-controlled suites. Blended powders are inline weighed, automated tub/pouch/stick filled, heat sealed, and lot coded.
Finished goods are tested against specification sheets. Upon QC release, COAs are issued and pallets are prepared for global freight shipping.
Direct Factory Quote & Consultation
Partner with Nutracap for cGMP-certified custom powder blending, unmatched flavor execution, low MOQs, and reliable lead times. Request a technical consultation and quote from our formulation team today.
Global Buyer FAQ & Search Intelligence
Comprehensive technical and commercial answers to key questions asked by international buyers, procurement managers, and brand founders.
Ingredient segregation (demixing) occurs when raw materials possess varying particle sizes, bulk densities, or particle shapes. Nutracap mitigates segregation through rigorous raw material mesh profiling and particle matching prior to compounding. For ultra-low dose active ingredients (e.g., micro-gram vitamins, trace minerals, or potent stimulants), we employ a multi-stage geometric dilution protocol (trituration) to ensure uniform active dispersion throughout the carrier matrix.
Our production cleanrooms utilize state-of-the-art ribbon and V-blenders calibrated for specific mass friction coefficients. Furthermore, every batch undergoes multi-point sampling (top, middle, and bottom blender locations) verified via High-Performance Liquid Chromatography (HPLC) or ICP-MS assay testing to guarantee 100% batch homogeneity before filling.
Nutracap offers some of the most competitive and flexible MOQs in the contract manufacturing industry. Our custom powder blending MOQs typically start at just 500 units for standard powder tubs, stand-up flexible pouches, or bulk drums. For specialized single-serve stick packs, MOQs depend on film yield but remain accessible for emerging brands.
This low entry threshold allows brand owners to pilot innovative formulations, test market demand, and scale up efficiently without tying up massive working capital in unsold inventory. As your brand grows, our automated lines seamlessly scale up to multi-thousand unit production runs.
Achieving outstanding palatability in functional powders requires sophisticated food chemistry. Raw materials like branched-chain amino acids (BCAAs), plant proteins (pea/hemp), ashwagandha, and caffeine carry naturally bitter, earthy, or astringent flavor profiles. Our in-house flavor lab addresses these challenges through three primary mechanisms:
Nutracap adheres strictly to US FDA 21 CFR Part 111 cGMP regulations. All raw ingredients received at our Norcross, GA facility are placed in quarantine until verified by our Quality Assurance laboratory. Our QA protocol includes:
Every finished batch is released with an official Certificate of Analysis (COA) documenting that the product meets all label claims and safety standards.
Once your custom powder formula is locked, flavor bench samples are approved, and label artwork is finalized, standard turnaround time is approximately 4 to 6 weeks. Lead times may vary based on custom ingredient availability (e.g., patented or specialized raw materials) and specialized packaging procurement.
Because Nutracap houses formulation, blending, container filling, label printing support, and packaging under a single facility roof in Georgia, we eliminate transit delays between separate vendors, guaranteeing fast and reliable delivery schedules.
Yes. Nutracap routinely manufactures and exports powder supplements for international brand owners across Europe, the Middle East, Latin America, Africa, and Asia-Pacific. We prepare complete export documentation packages, including:
We offer a comprehensive selection of primary and secondary packaging options tailored to your sales channels (retail store shelves, Amazon FBA, DTC e-commerce, or clinical distribution):
You retain 100% ownership of your proprietary custom formula. Before detailed ingredient selection or flavor bench work begins, Nutracap signs a comprehensive Non-Disclosure Agreement (NDA) to protect your intellectual property, flavor profiles, and business strategies. We maintain absolute confidentiality regarding all your brand specifications.