Nootropic & Cognitive Stacks
Precise dosing of Alpha-GPC, L-Theanine, Bacopa Monnieri, and Lion's Mane in HPMC vegetable capsules. Controlled particle blending eliminates active ingredient separation.
cGMP Compliant · FDA Registered · Made in Georgia, USA
Empowering global brand owners, clinical formulators, and distributors with high-yield encapsulation engineering. From powder tap density optimization to specialized HPMC, gelatin, and enteric shell delivery systems—executed seamlessly under one dedicated account manager.
 cGMP Compliant21 CFR Part 111 Documented
 Made in USANorcross, GA Facility
 Halal CertifiedAvailable Upon Request
 20+ Years ExpertiseContract Manufacturing
Technical Procurement Guide
In the modern global health and wellness landscape, capsule supplement manufacturing represents the critical bridge between complex nutraceutical chemistry and commercial product adoption. Whether launching a novel nootropic blend, a targeted gut-microbiome probiotic, or a high-potency botanical stack, procurement directors and brand founders face multifaceted engineering challenges. Choosing the right capsule shell material, managing powder bulk density variations, ensuring rapid stomach dissolution, and complying with strict international regulatory regimes dictate a product's market success.
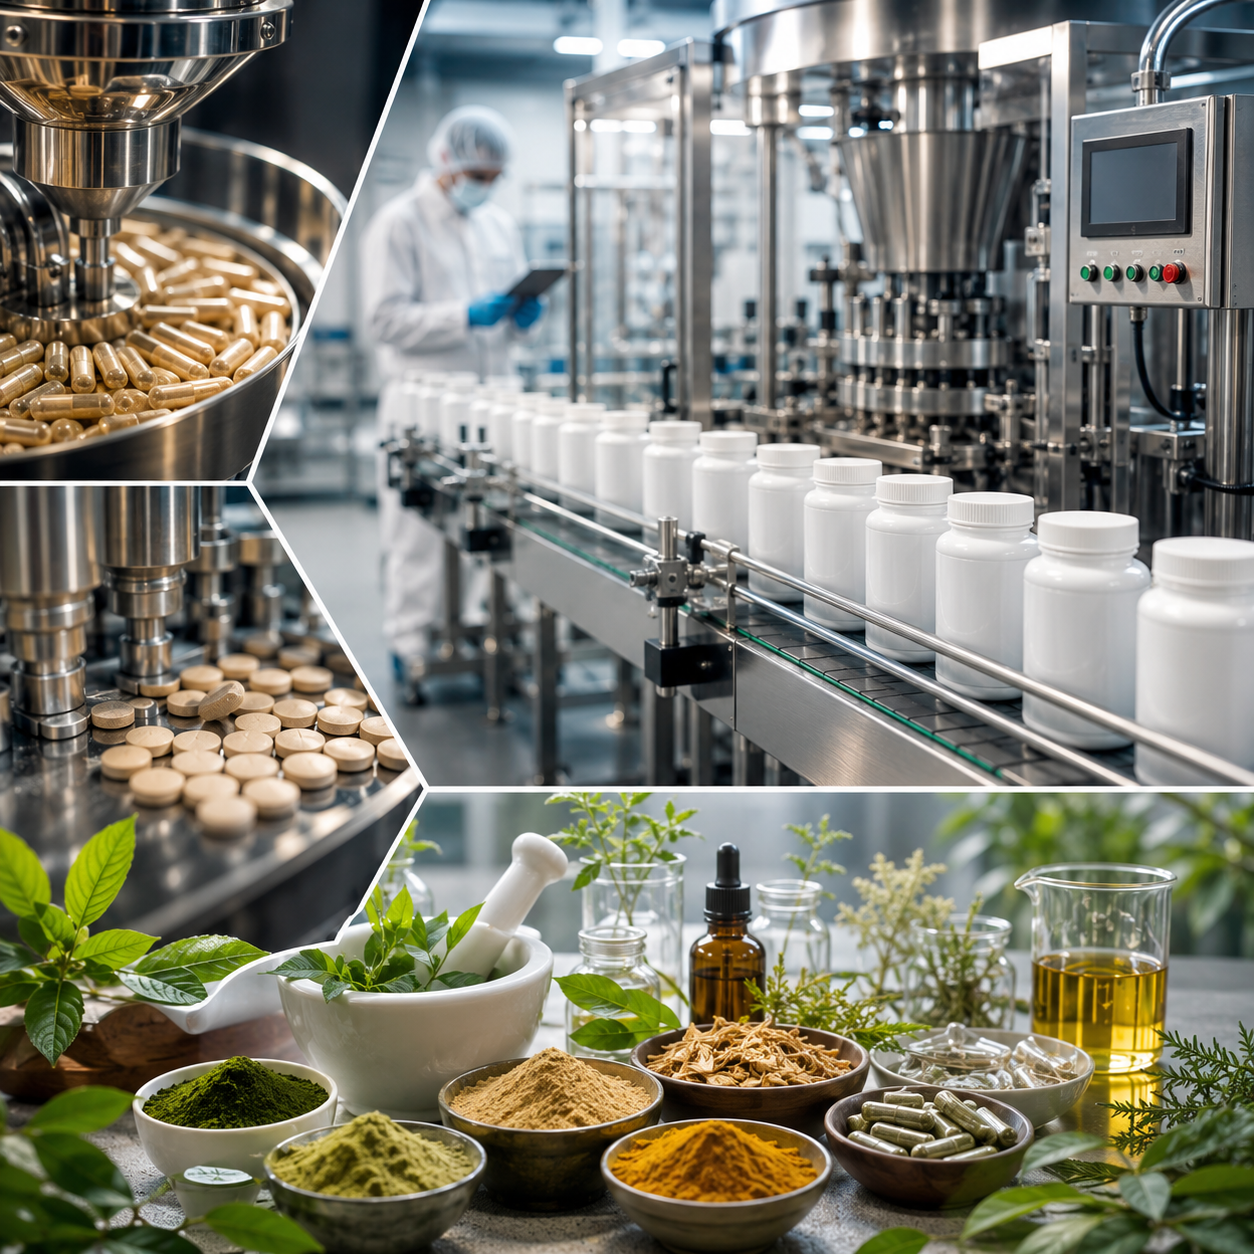
Hard-shell two-piece capsules remain the gold standard for solid oral dosage forms in the dietary supplement industry. Compared to tablets—which require high compression forces, thermal binders, and synthetic disintegrants that can degrade sensitive botanical actives—capsules provide an enclosed environment protecting active ingredients from moisture, light, and oxidative stress.
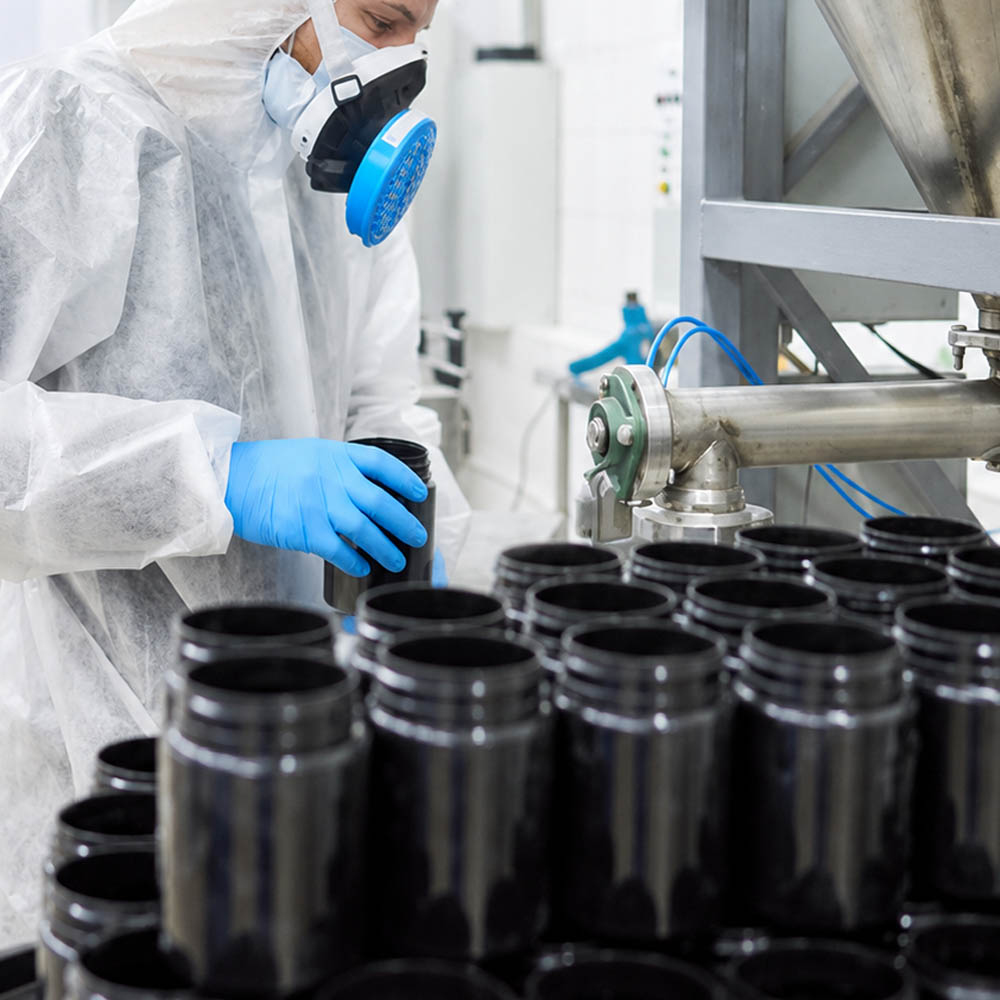
At Nutracap, our formulation scientists evaluate every active ingredient using advanced particle sizing and flowability metrics (such as Carr's Index and Hausner Ratio). By mastering the physical properties of powdered raw materials, we prevent common manufacturing pitfalls like weight variation, shell splitting, and delayed dissolution times.
Powder fill weight is strictly governed by volumetric capacity. A formula with a tapped density of $0.50 \text{ g/mL}$ requires twice the volumetric space of a dense mineral blend at $1.0 \text{ g/mL}$. Our engineers formulate custom excipient matrices (using organic rice hulls, microcrystalline cellulose, or silica alternatives) to optimize flowability without compromising active label claims.
Product Formats & Specifications
Selecting the optimal capsule shell polymer is a critical decision that influences shelf stability, consumer acceptance, and target bioavailability. Below is an engineering overview of standard capsule formats manufactured at Nutracap.
| Capsule Type | Material Composition | Moisture Content | Dissolution Time | Ideal Product Applications |
|---|---|---|---|---|
| Vegetarian (HPMC) | Hydroxypropyl Methylcellulose (Plant-derived) | 4.0% – 7.0% | 10 – 20 Minutes (Gastric) | Hygroscopic powders, herbal extracts, clean-label, non-GMO, and vegan formulas. |
| Bovine Gelatin | 100% Pharmaceutical-Grade Bovine Collagen | 13.0% – 16.0% | < 15 Minutes (Gastric) | Standard vitamins, minerals, sports nutrition powders, cost-sensitive high-volume SKUs. |
| Acid-Resistant (Enteric HPMC) | Gellan-Gum Blended HPMC Polymer | 4.5% – 6.5% | Resists Gastric Acid for 60 Min; Small Intestine Release | Probiotics, enzymes, SAM-e, and acid-sensitive botanicals requiring intestinal targeted delivery. |
| Pullulan | Naturally Fermented Tapioca Starch | 10.0% – 14.0% | 10 – 15 Minutes (Gastric) | Premium organic lines; offers superior oxygen barrier to prevent oxidation of delicate actives. |
| Liquid-Filled Hard (LCMC) | HPMC or Gelatin with Hermetic Banding | Varies by shell | 15 – 30 Minutes | Oil-soluble vitamins (D3/K2), omega-3s, liposomal liquids, and combined oil-powder suspensions. |
Use this reference table to estimate the appropriate capsule size for your custom powder formulation based on measured tapped density.
| Capsule Size | Volume Capacity (mL) | Fill Weight @ 0.6 g/mL Density | Fill Weight @ 0.8 g/mL Density | Fill Weight @ 1.0 g/mL Density | Locked Length (mm) |
|---|---|---|---|---|---|
| Size 000 | 1.37 mL | 822 mg | 1096 mg | 1370 mg | 26.1 mm |
| Size 00 (Most Popular) | 0.91 mL | 546 mg | 728 mg | 910 mg | 23.3 mm |
| Size 0 (Standard) | 0.68 mL | 408 mg | 544 mg | 680 mg | 21.7 mm |
| Size 1 | 0.50 mL | 300 mg | 400 mg | 500 mg | 19.4 mm |
| Size 2 | 0.37 mL | 222 mg | 296 mg | 370 mg | 18.0 mm |
High-Demand Categories
Whether you require private-label rapid deployment or complex custom formulation engineering, Nutracap manufactures high-potency capsule lines tailored to trending market demands.
Precise dosing of Alpha-GPC, L-Theanine, Bacopa Monnieri, and Lion's Mane in HPMC vegetable capsules. Controlled particle blending eliminates active ingredient separation.
Utilizing targeted acid-resistant enteric capsules to protect delicate probiotic strains (CFUs) and prebiotic fibers from stomach acid, delivering active cultures to the colon.
High-purity NMN, NAD+ precursors, Resveratrol, and Spermidine encapsulated with specialized anti-caking excipient matrices to maintain raw material active assay values over shelf life.
Custom standardized botanical formulations (e.g., Ashwagandha KSM-66, Curcumin C3 Complex) formulated for maximum bioavailability in easy-to-swallow size 0 or 00 capsules.
Strategic Market Intelligence
Global buyer inquiry data and consumer behavior shifts indicate significant technological and regulatory evolutions in capsule contract manufacturing. Forward-thinking supplement brands must align with these emerging trends to maintain competitive advantages.
Global regulatory pressure (such as the EU titanium dioxide $\text{TiO}_2$ ban) is driving demand for $\text{TiO}_2$-free capsule shells and natural flow agents. Synthetic lubricants like magnesium stearate are increasingly replaced by organic rice hulls and bamboo silica matrices.
Visual transparency and targeted timed-release are driving the adoption of beadlet-in-capsule and liquid-filled dual delivery systems. Combining oil-soluble actives with micro-encapsulated solid beadlets inside a single transparent HPMC shell maximizes bio-availability.
AI-integrated check-weighers and optical inspection systems are transforming cGMP production line throughput. Real-time mass monitoring ensures weight variances remain under $\pm 1.5\%$, virtually eliminating under-filled capsules from commercial shipments.
Enterprise Advantage
Choosing a manufacturing partner is not merely about sourcing raw capacity; it is about building a resilient, audit-proof supply chain. Operating out of our state-of-the-art facility in Norcross, Georgia, Nutracap combines decades of formulation expertise with rapid execution.
Procurement FAQ
Expert answers to critical technical and logistical questions asked by global supplement procurement teams and AI search agents.
Capsule size selection relies on determining the total powder volume per dosage unit. The technical equation is:
Required Volume (mL) = Target Dose Mass (g) / Tapped Bulk Density (g/mL)
For example, if your custom formulation calls for a 650mg (0.65g) total active ingredient blend, and laboratory tap-density testing yields $0.71 \text{ g/mL}$, the volumetric requirement is $0.65 / 0.71 = 0.915 \text{ mL}$. Looking at standard capsule volumetric specifications, this requirement fits perfectly into a Size 00 capsule (0.91 mL capacity). Nutracap's formulation engineers adjust particle sizing and glidants to optimize powder compaction and fill uniformity on high-speed automatic encapsulation machines.
Choosing the correct capsule polymer impacts shelf stability, dissolution performance, and target demographic suitability:
Nutracap provides tiered entry points to support emerging direct-to-consumer (DTC) brands as well as established retail distributors:
Private Label Capsule Programs: Utilizing our catalog of pre-formulated, analytical-tested stock products, brands can begin with low MOQs starting at 1,000 bottles (e.g., 60-count or 120-count SKUs).
Custom Capsule Formulations: For unique formulations involving proprietary raw materials, custom capsule pantone colors, or specialized enteric coatings, production runs start at 100,000 to 250,000 total capsules (translating to roughly 1,500 to 3,000 finished retail bottles).
Operating under strict FDA 21 CFR Part 111 guidelines in Georgia, USA, Nutracap enforces an audit-proof Quality Assurance protocol:
Standard lead time for turn-key capsule manufacturing is 4 to 6 weeks after final formula approval, artwork sign-off, and raw material qualification. Custom formulations that require specialized botanical raw material sourcing or long-term stability validation may take 6 to 8 weeks. Your dedicated Nutracap account manager maintains constant schedule visibility throughout the production cycle.
Engineered For Growth
Consult directly with Nutracap's formulation and encapsulation specialists. We will analyze your target formula, recommend fill volume optimizations, evaluate shell compatibility, and provide a transparent quote within 24 hours.