cGMP Certified Packaging · Made in GA, USA
High-Performance Supplement Packaging Solutions for Global Brand Scale
From moisture-vapor barrier engineering and induction-sealed PET/HDPE bottles to single-serve stick packs and PCR eco-resins—we safeguard formula integrity while maximizing retail velocity.
- FDA 21 CFR Part 111 cGMP Compliant Bottling, Powder Filling & Blister Packaging
- Active barrier protection (Low MVTR & OTR metrics) for maximum active potency retention
- Turnkey label design, FDA compliance review, and automated batch traceability
-
 cGMP CompliantAudited batch control
-
 Made in the USANorcross, Georgia plant
-
 Halal CertifiedInternational compliance
-
 Accredited Enterprise20+ years of expertise
Strategic Packaging Engineering
Why Advanced Supplement Packaging Solutions Define Brand Equity
In the global dietary supplement sector, container closure systems are far more than aesthetic vessels—they represent the vital physical barrier protecting active ingredient potency against environmental degradation. Brand owners, contract buyers, and institutional importers face mounting pressures: stringent FDA regulatory scrutiny, escalating cross-border supply chain stresses, and demanding consumers who expect sustainable, tamper-evident packaging.
Nutracap approaches packaging through a combined lens of material science, pharmaceutical compliance, and shopper psychology. Whether housing delicate live probiotic strains, hygroscopic herbal extracts, or high-volume whey protein isolates, our contract packaging infrastructure in Norcross, Georgia delivers engineered reliability.
- Polymer Science Optimization: Balancing MVTR (Moisture Vapor Transmission Rate) and OTR (Oxygen Transmission Rate) for extended stability.
- Tamper-Evident & Child-Resistant Engineering: Induction heat sealing, shrink banding, and CR-certified closures compliant with US CPSC standards.
- Seamless Turnkey Integration: In-house graphic design, Supplement Facts panel auditing, and high-speed robotic packing under one roof.
Material Science Breakdown
Packaging Substrate Comparison Matrix
Selecting the optimal container material requires evaluating moisture permeability, oxygen ingress resistance, UV filtration, and structural rigidity against formulation requirements.
| Packaging Substrate | Moisture Barrier (MVTR) | Oxygen Barrier (OTR) | UV Light Protection | Primary Recommended Dosage Forms | Sustainability Profile |
|---|---|---|---|---|---|
| HDPE (High-Density Polyethylene) | Superior (< 0.3 g/m²/day) | Moderate | High (Opaque options) | Capsules, Tablets, Moisture-Sensitive Powders | 100% Recyclable (Code 2), High PCR Availability |
| PET (Polyethylene Terephthalate) | Good | Excellent (< 5.0 cc/m²/day) | Moderate (Amber/Cobalt Tinted) | Gummies, Softgels, Liquids, Clear Tubs | 100% Recyclable (Code 1), rPET Compatible |
| Flexible Multi-Layer Laminates (PET/ALU/PE) | Maximum (< 0.01 g/m²/day) | Maximum (< 0.01 cc/m²/day) | Total Photoprotection (100%) | Single-Serve Stick Packs, Protein Pouches, Sachets | Mono-material recyclable variants emerging |
| Alu-Alu Cold-Form Blisters | Absolute Hermetic Seal | Absolute Hermetic Seal | Total Photoprotection (100%) | Probiotics, High-Value Actives, Softgels | Specialized recycling streams required |
| Amber Glass Containers | Absolute Barrier | Absolute Barrier | High UV Spectrum Blocking | Sublingual Drops, Oils, Specialty Liquids | Infinitely Recyclable, Premium Weight Impact |
Product Recommendations
Core Supplement Packaging Formats Engineered by Nutracap
We provide tailored container formats configured for high-speed automated packaging lines, ensuring pristine product presentation and extended shelf life.
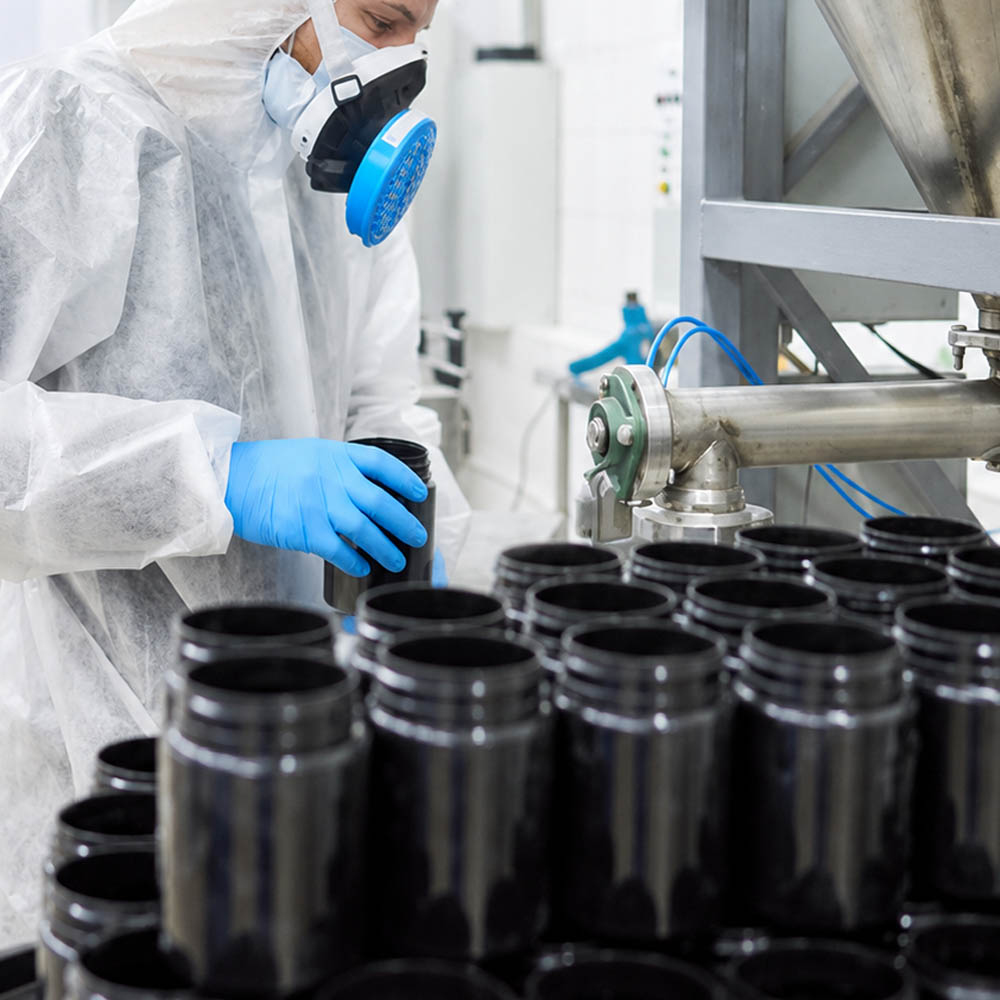
Pharmaceutical-Grade Bottles & Jars
Precision-molded HDPE, PET, and Glass bottles in Packer, Wide-Mouth, and Boston Round profiles (60cc to 1000cc). Equipped with heat-induction foil seals and child-resistant closures.
View Bottle Specs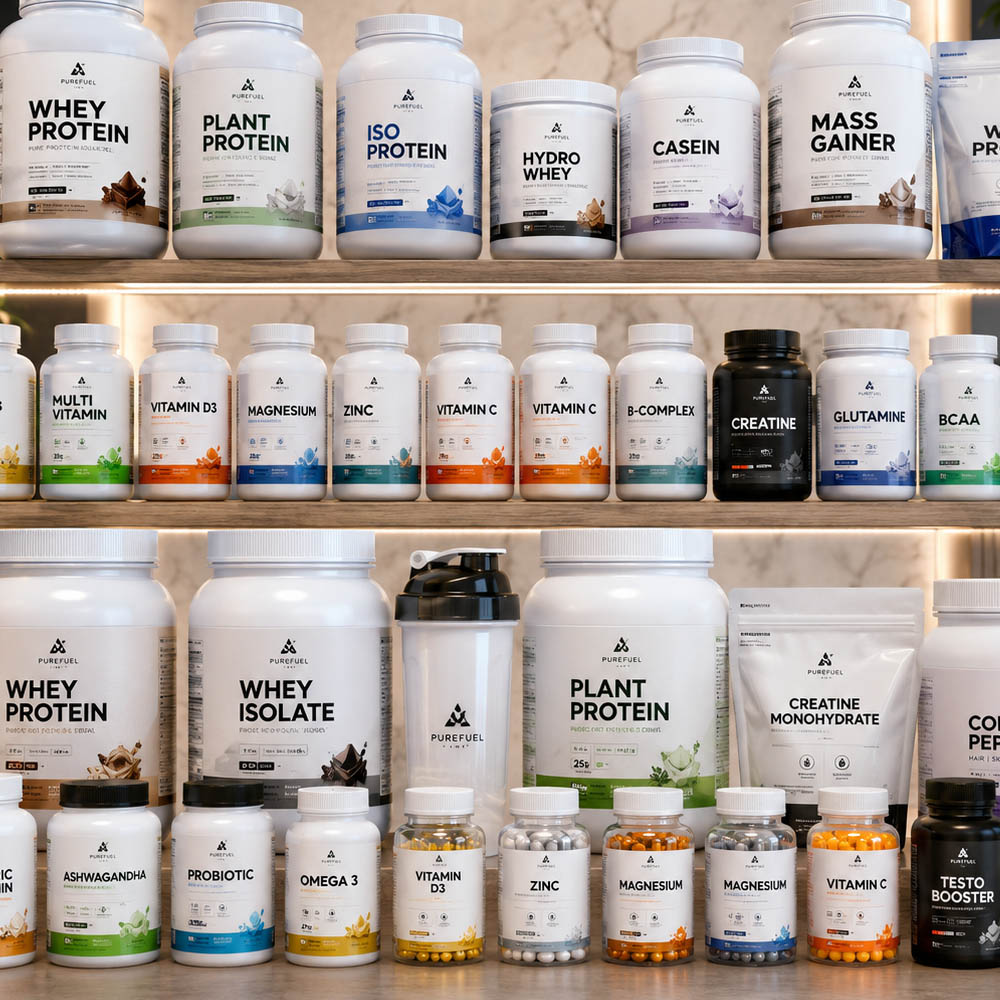
Powder Tubs & Stand-Up Pouches
Rigid HDPE/PET tubs with scoop-holding neck rings alongside flexible stand-up pouches (Doypack) featuring press-to-close zippers and high-barrier metallized film structures.
View Powder Packaging
Single-Serve Stick Packs & Sachets
High-speed narrow-format stick packaging for hydration powders, pre-workouts, and greens. Nitrogen flushed to prevent active oxidation and active ingredient clumping.
Stick Pack Solutions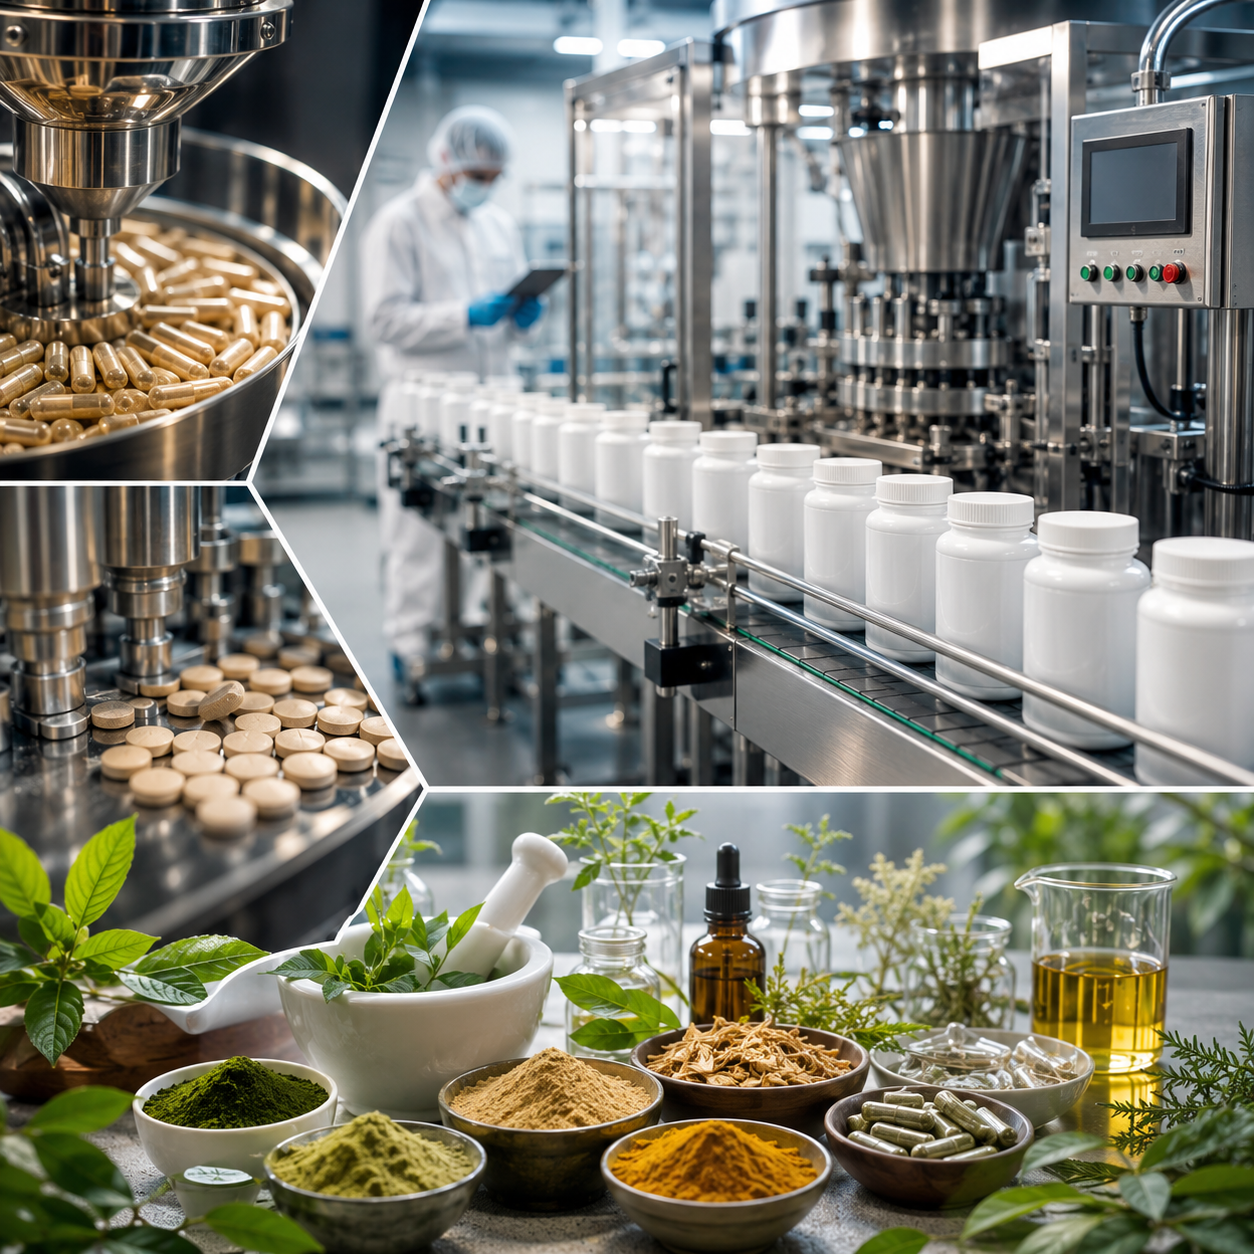
Blister Packs (Thermoformed & Cold-Form)
Individual cavity isolation utilizing PVC/PVDC or Alu-Alu (Aluminum/Aluminum) structures. Provides superior moisture protection for probiotics and premium clinical formulas.
Blister Packaging SpecsStrategic Horizon
The Future of Supplement Packaging: 2026–2030 Trends
Global buyer preferences are shifting rapidly under the influence of regulatory changes, environmental mandates, and AI-driven supply chains. Here is how modern brands stay ahead.
1. Transition to High-Ratio PCR & Bio-Resins
Global regulations (such as EU packaging directives and US state-level mandates) increasingly penalize virgin plastics. Modern brands are adopting 30% to 100% Post-Consumer Recycled (PCR) HDPE and rPET bottles, which reduce greenhouse gas footprints while preserving food-contact safety standards.
2. Smart Packaging & Digital Traceability
Integrating 2D DataMatrix codes, dynamic QR systems, and NFC chips directly onto primary labels enables instantaneous consumer authentication, lab-analysis transparency (COAs), supply chain anti-counterfeiting, and personalized dosage tracking directly via mobile devices.
3. Active & Intelligent Moisture Management
Traditional desiccant packets are giving way to desiccant-lined closures, active oxygen-scavenging resin additives, and molecular sieve neck inserts. These engineering advancements maximize active shelf life without compromising automated filling speeds.
4. E-Commerce & SIOC Optimization
With direct-to-consumer sales expanding globally, packaging must pass Amazon SIOC (Ships-In-Own-Container) and ISTA-6 integrity standards. Modern packaging design focuses on crush-resistant wall thickness, leak-proof induction seals, and weight-optimized geometries to reduce dimensional freight penalties.
5. Monomaterial Recyclable Flexible Packaging
Historical flexible pouches used non-recyclable multi-material layers (PET/Foil/PE). Modern polymer developments allow high-barrier All-PE (Polyethylene) pouch structures that qualify for store drop-off recycling streams without sacrificing moisture vapor barriers.
6. Custom Tactile & Sensory Retail Branding
As retail shelves grow increasingly crowded, brands rely on premium embellishments: soft-touch matte lamination, spot UV, metallic cold-foil accents, embossed logos, and custom-molded ergonomic bottle caps to command premium pricing.
Technical Advice for Institutional Procurement
When engineering high-volume product lines, container selection should occur simultaneously with formulation design. Hygroscopic botanical powders (such as Ashwagandha or Mushroom extracts) require strict MVTR containment below 0.1 g/m²/day to prevent caking, whereas liposomal liquids require precise oxygen scavenging to preserve lipid stability.
Contact Us to consult directly with our packaging engineers on stability and barrier requirements.
Quality Assurance Workflow
5-Stage cGMP Packaging Execution Protocol
Every packaging run at Nutracap follows documented standard operating procedures (SOPs) to ensure lot uniformity, weight accuracy, and total seal integrity.
Component Testing
Primary containers, closures, and inner seals undergo incoming lot inspection for dimensions, cleanliness, and food-contact compliance (21 CFR Part 177).
Automated Line Setup
High-speed bottle unscramblers, desiccators, electronic tablet/capsule counters, and powder auger fillers are calibrated for zero product giveaway.
Induction & Cap Sealing
Containers pass through high-frequency electromagnetic induction cappers to weld aluminum foil inner seals, establishing an air-tight barrier.
Labeling & Vision Check
Precision pressure-sensitive labeling equipment applies artwork; automated camera vision systems verify barcode readability, lot codes, and expiration dates.
Case Packing & COA Release
Finished goods are cartoned, shrink-wrapped on heavy-duty pallets, and held in quarantine until Quality Assurance releases the Certificate of Analysis (COA).
Why Choose Nutracap
The Nutracap Advantage in Contract Supplement Packaging
Nutracap is not a broker or middleman. We operate a state-of-the-art, FDA-registered, cGMP-compliant manufacturing and packaging facility in Norcross, Georgia. By consolidating raw material blending, encapsulation, bottling, and label compliance under one roof, we eliminate multi-vendor friction and accelerate time-to-market.
- Dedicated Account Management: One direct point of contact overseeing your project from engineering to final freight dispatch.
- Full FDA Regulatory & Label Assurance: In-house review of Supplement Facts panels, active claims, allergen disclosures, and net weight formatting.
- Global Market Authorization: Complete documentation package including Certificate of Free Sale, Halal Certification, and full batch records for international customs clearance.
- Agile Scalability: Low MOQs for emerging brand launches (starting at 1,000 units), with infrastructure engineered to scale to millions of units seamlessly.
Comprehensive Solutions
Popular Supplement Packaging Categories
Explore specialized container and finishing formats manufactured inside our Georgia plant.
Start Your Packaging Project
Ready to Upgrade Your Brand’s Supplement Packaging?
Connect with a senior packaging strategist at Nutracap. We will analyze your formula specifications, target shelf life, barrier requirements, and provide a competitive quotation within 24–48 hours.
Technical B2B FAQ
Frequently Asked Questions on Supplement Packaging Solutions
Get immediate clarity on material selection, barrier physics, regulatory guidelines, and production lead times.
HDPE (High-Density Polyethylene) provides superior moisture barrier properties (low MVTR) and high structural rigidity with high opacity, making it ideal for hygroscopic powders, sensitive botanical extracts, tablets, and capsules. PET (Polyethylene Terephthalate) offers exceptional glass-like clarity, high impact resistance, and a strong barrier against oxygen (low OTR), making it preferred for aesthetic retail products, clear gummies, softgels, and liquid supplements. Our engineers will guide you based on your formula's specific moisture sensitivity.
Moisture Vapor Transmission Rate (MVTR) and Oxygen Transmission Rate (OTR) determine shelf-life stability. Probiotics, effervescent powders, and hygroscopic botanical extracts require ultra-low MVTR packaging (<0.05 g/m²/day) and near-zero OTR. This is achieved using high-barrier multi-layer aluminum foil laminates, desiccant-integrated closure caps, or Alu-Alu cold-form blisters combined with nitrogen flushing during high-speed filling to preserve active Colony Forming Units (CFUs).
Yes. Every automated bottling line at Nutracap includes inline high-frequency induction foil sealing to create a hermetic air-tight seal, preserving formula potency and providing consumer tamper verification. We also offer custom-printed tamper-evident full-body shrink sleeves, perforated neck bands, and pressure-sensitive seals compliant with US CPSC and global retail safety requirements.
Post-Consumer Recycled (PCR) resins such as 30% to 100% rPET or rHDPE offer comparable structural integrity to virgin plastics when sourced from food-grade certified supply chains. Nutracap conducts real-time and accelerated stability testing to ensure PCR barrier properties maintain chemical inertness, prevent leachables, and protect active potencies over the full 24-to-36 month shelf life.
Under FDA 21 CFR Part 111 (cGMP for Dietary Supplements) and 21 CFR Part 177 (Indirect Food Additives), primary packaging materials must be food-contact safe, non-reactive, non-additive, and non-absorptive. Container closure systems must protect against physical contamination, light degradation, and moisture intrusion while maintaining compliant Supplement Facts panel layouts, allergen declarations, lot numbers, and expiration dating.
Yes. We specialize in international contract packaging. We handle multi-lingual label layouts, regional compliance adjustments (such as EFSA, UAE-S, or TGA guidelines), barcoding standards (EAN/GS1), and supply essential export documentation including Certificates of Free Sale, cGMP Certificates, Halal Certificates, and Certificates of Analysis (COA) for smooth customs clearance.
Nutracap offers low entry-level MOQs starting at 1,000 bottles for private label programs and 500 units for standard powder tubs. Custom high-barrier film pouches or specialized custom plastic molds typically start at 5,000 to 10,000 units. Turnkey turnaround times range between 4 to 6 weeks from label artwork and component approval.