Explore our high-performance adhesive labels, cosmetic packaging, organic sheet masks, personal care formulations, and customized apparel packaging designed for global compliance and shelf dominance.
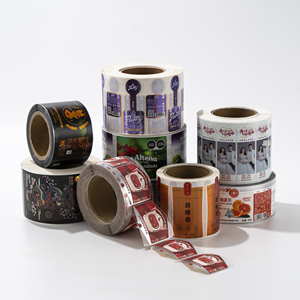
In today's highly competitive commercial ecosystem, product labeling has evolved far beyond a basic regulatory requirement; it stands as the critical touchpoint of brand equity, consumer trust, and supply chain integrity. As a Top Trusted Label Design Manufacturer & Exporter, our manufacturing infrastructure bridges advanced polymer chemistry, high-definition digital/flexographic hybrid printing, and stringent global regulatory compliance.
Modern retail landscapes demand label substrates engineered to survive hostile environments—ranging from deep-freeze cold chains (-40°C) for specialized dietary supplements and bio-serums, to high-humidity bathroom environments for organic skincare and personal care packaging. According to recent market analysis, brands that transition from standard paper packaging to custom-engineered, tactile-varnished, and UV-resistant synthetic labels experience up to a 34% increase in first-impression retail conversions.
Our state-of-the-art facility operates under strict cGMP standards and FDA registration, serving enterprise clients across North America, Europe, Asia-Pacific, and the Middle East. By integrating raw material identity testing, automated inline spectroradiometric color verification, and 100% batch lot traceability, we guarantee that every label roll, pressure-sensitive sticker, and custom packaging solution delivers flawless brand consistency and long-term durability.
Understanding user search intent and market shifts: How sustainable substrates, smart labeling technology, and strict FDA/EU regulatory enforcement are reshaping global procurement decisions.
Global consumer demand is rapidly driving brand adoption of Post-Consumer Recycled (PCR) plastics, biodegradable PLA films, and FSC-certified bamboo papers. Sourcing managers now prioritize supplier partners capable of delivering recyclable pressure-sensitive adhesives that leave zero residue during container washing and reprocessing cycles.
To combat counterfeit pharmaceuticals, luxury cosmetics, and premium nutraceuticals, top exporters are embedding ultra-thin RFID/NFC chips directly between label face sheets and liner backings. This enables real-time supply chain tracking, anti-tamper security validation, and interactive consumer digital engagements.
Regulatory authorities including the FDA (21 CFR 101.9), EFSA, and GCC customs strictly enforce precise format structures for Supplement Facts, Drug Facts, and INCI cosmetic ingredient declarations. Manufacturers offering in-house legal label auditing prevent costly port rejections and retail pull-backs.
Select the optimal label material engineered for your specific product category, container material, and environmental exposure conditions.
| Label Substrate Material | Primary Application Areas | Adhesive System | Temperature Range | Water & Oil Resistance | Special Finishes |
|---|---|---|---|---|---|
| BOPP (White / Clear / Metallic) | Cosmetics, Food & Beverage, Supplements | Permanent Acrylic / Removable | -20°C to +80°C | 100% Waterproof / Oil-Proof | Matte/Gloss Lamination, Cold Foil Stamping |
| Cast Coated Ultra Paper | Wine Bottles, Gourmet Food, Vitamin Jars | Emulsion Acrylic / Cold Glue | -10°C to +60°C | Moderate (Requires Varnish) | Embossing, Debossing, Hot Foil Stamping |
| Direct Thermal & Thermal Transfer | Logistics, Barcode Shipping, Outer Cartons | Permanent Rubber / Hot Melt | -40°C to +50°C | Low to Medium | UV Coated Protection, Variable Data Printing |
| Biodegradable PLA Film | Organic Skincare, Sustainable Apparel, Snacks | Eco-Friendly Compostable Adhesive | -15°C to +50°C | High Water Resistance | Soy-based Inks, Soft Touch Matte Coating |
| Heavy-Duty Vinyl (PVC / PET) | Chemical Drums, Outdoor Equipment, Auto | High-Tack Solvent Acrylic | -40°C to +120°C | Extreme Chemical & UV Immunity | Scratch-Resistant Polycarbonate Overlaminate |
Operating out of our advanced USA-based production facility in Georgia, our integrated manufacturing model eliminates reliance on fragmented sub-contractors. Whether you require private label dietary supplement bottles, custom printed vinyl adhesive rolls, luxury cosmetics packaging, or customized jacquard apparel tags, our end-to-end production workflow guarantees unbeatable speed-to-market.
Because our engineering teams oversee chemical formulations, container sourcing, and label printing under one roof, we solve technical incompatibilities—such as container outgassing or adhesive flagging—before mass production commences.
Our certified regulatory specialists review all Supplement Facts panels, INCI skincare ingredients, net content disclosures, and allergen warnings against current FDA and international customs standards prior to plate making.
We support fast-growing digital brands with low minimum order quantities (starting from 500–1,000 units for private label launches) while possessing the high-speed rotary flexographic capacity to output millions of roll labels daily.
Every project is assigned a dedicated technical account manager who coordinates prepress proofing, raw material sourcing, sample bench testing, and international freight documentation for seamless delivery.
As global logistics routes diversify and e-commerce platforms enforce stricter packaging mandates (such as Amazon Ships in Own Container - SIOC), label design must continuously adapt. Key technical breakthroughs currently implemented across our manufacturing lines include:
Clear, authoritative answers to common enterprise procurement inquiries regarding MOQs, lead times, regulatory compliance, and export documentation.
Ready to elevate your product line with high-precision custom labels, compliant packaging, and scalable manufacturing? Request a direct consultation with our technical specialists today.
Contact Us