Explore our core spectrum of analytical testing machinery, quality verification kits, dietary supplement inspection services, and OEM sample developments.
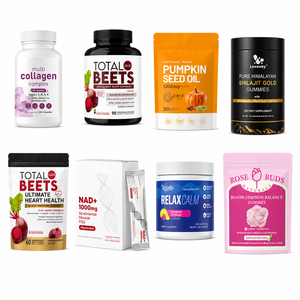
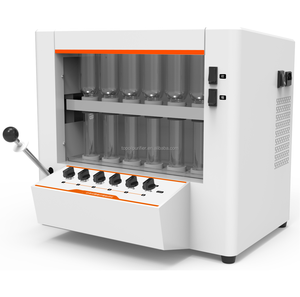
Why leading global healthcare brands choose our China manufacturing and independent laboratory testing ecosystem.
Our analytical laboratories utilize High-Performance Liquid Chromatography (HPLC) and Mass Spectrometry to verify potent active ingredients, plant extract standardization, and vitamin purity down to parts-per-billion (ppb) sensitivity.
Inductively Coupled Plasma Mass Spectrometry (ICP-MS) safeguards products against Lead, Cadmium, Arsenic, and Mercury contamination. Rigorous USP <61/62> micro panels eliminate pathogens prior to batch release.
Equipped with environmental chambers complying with ICH Q1A(R2) guidelines. We execute accelerated (40°C/75% RH) and real-time stability studies to establish precise shelf-life, active degradation curves, and dissolution rates.
The global dietary supplement market is experiencing a paradigm shift. Consumers, regulatory bodies such as the US FDA, EFSA, and China's SAMR, alongside major e-commerce marketplaces (including Amazon's strict ISO 17025 verification policy) demand unprecedented chemical verification, formula stability, and raw material traceability. As a top China supplement testing manufacturer and factory group, our integrated operations unify state-of-the-art analytical testing equipment, standardized batch production, and third-party laboratory verification into a seamless contract manufacturing framework.
In modern dietary supplement production, quality control is no longer a post-production checkpoint; it is embedded across the raw material life-cycle. China's leading supplement testing factories employ advanced instrumental analytical chemistry to eliminate adulteration, guarantee active ingredient dosages, and prevent physical gel/capsule degradation.
| Testing Parameter | Analytical Methodology | Standard Reference Limit | Operational Target |
|---|---|---|---|
| Active Assay Potency | HPLC-DAD / LC-MS/MS | USP / EP / ChP Specifications | 100% – 105% of Label Claim |
| Heavy Metals (Pb, Cd, As, Hg) | ICP-MS (USP <233>) | FDA / EU 2023/915 Limits | < 0.1 ppm Trace Levels |
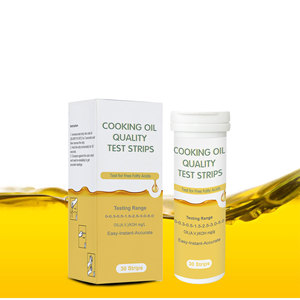
| Free Fatty Acids (FFA) | Titrimetric / Acid Strips | Commercial Grade Limits | < 1.0% Oleic Acid Equivalent |
| Microbial Enumeration | USP <61> / <62> Automated Culture | BAM / USP Clean Limits | Zero Pathogens (Salmonella/E.coli) |
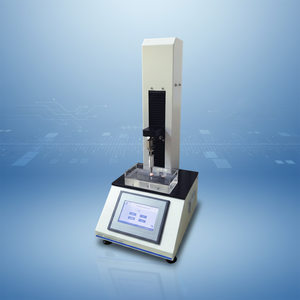
| Softgel Shell Burst Force | Mechanical Load Transducer | Internal SOP Specs | > 10.0 N Resistance Strain |
A comprehensive China contract manufacturing partner delivers full-spectrum formulation pathways customized for global brand owners. Whether scaling private-label immunity trial kits or engineering complex multi-phase release capsules, production processes adhere strictly to Current Good Manufacturing Practices (cGMP).
A. Fish Oil & Fat-Soluble Softgels: Sourcing high-purity concentrates requires precise nitrogen purging throughout manufacturing to safeguard unsaturated double bonds against oxygen exposure. Advanced softgel encapsulation lines maintain precise gel-ribbon thickness and thermal sealing tolerances, guaranteeing structural uniformity across multi-million capsule runs.
B. Precision Powder Blending & Botanical Extracts: Granulation, particle sizing, and high-efficiency ribbon blending ensure uniform distribution of micro-ingredients (such as Vitamin D3, Chromium Picolinate, or active botanical extracts). In-process sample testing monitors moisture content (LOD) and tap density to maintain capsule fill consistency.
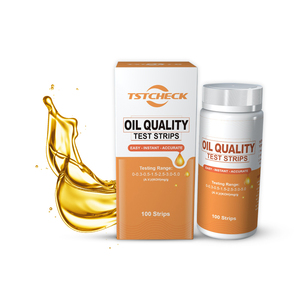
C. Analytical Test Strip & Rapid Field Kit Manufacturing: Beyond traditional dosage forms, leading factories engineer diagnostic test strips and chemical verification indicators. These custom OEM diagnostic tools empower commercial kitchens, food manufacturers, and health-conscious consumers to instantly analyze oil degradation and chemical purity.
Strategic purchasing managers must align their supply chains with evolving technological, regulatory, and market vectors. The future of nutraceutical procurement revolves around five dominant trends:
Regulatory frameworks are tightening worldwide. The European Union's updated contaminant threshold regulations (such as strict ethylene oxide, PAHs, and pyrrolizidine alkaloid monitoring) coupled with US FDA FSVP requirements mandate that Chinese manufacturing facilities operate with complete analytical transparency.
Forward-thinking factories are embedding Near-Infrared (NIR) inline sensors directly into high-speed powder blenders. This NIR technology provides real-time homogeneity data, terminating the mixing cycle precisely when statistical uniformity is achieved. Furthermore, continuous accelerated stability testing chambers provide longitudinal data that supports valid shelf-life claims in varied climatic zones (Zone IVb hot and humid conditions).
We bridge the gap between rigorous scientific validation and cost-efficient OEM manufacturing capacity.
Full support for international customs clearance documentation, including Certificate of Free Sale (CFS), Halal Certification, Kosher Compliance, US FDA Facility Registration, and full lot-traceability dossiers.
Our senior pharmaceutical chemists refine your target formula to resolve active ingredient incompatibilities, enhance bioavailability, reduce capsule size, and optimize organoleptic flavor profiles for powders.
We execute strict Non-Disclosure Agreements (NDAs) prior to formula disclosure. Your proprietary ingredient ratios, custom flavor codes, and trade secrets remain fully protected under intellectual property safeguards.
Clear technical and commercial answers for purchasing executives, quality managers, and healthcare brand owners.
Transform your product vision into scientifically verified, market-ready dietary supplements. Contact our technical engineering and procurement specialist team today.