Explore our high-capacity contract production capabilities spanning premium whey protein powders, advanced nutraceutical delivery systems, and complete private label retail packaging portfolios.
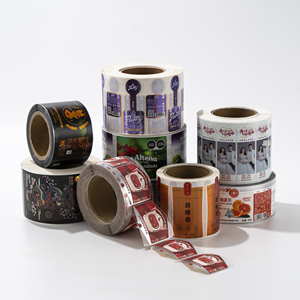
FDA-compliant, water-resistant high-barrier adhesive labeling engineered specifically for protein tubs, pouch packaging, and supplement containers.
Get a Quote
Precision tableting and direct-to-consumer private label branding for innovative solid chewable supplement lines and specialty oral care actives.
Get a Quote
Full-service custom apparel manufacturing to accompany sports nutrition brand product launches, promotional kits, and VIP gym bundles.
Get a Quote
cGMP-manufactured topical skin nutrition formulations infused with bioactive botanical extracts, green tea mud, and organic tea derivatives.
Get a Quote
Advanced topical emulsion formulation engineered for hyperpigmentation correction, skin barrier repair, and deep epidermal hydration.
Get a Quote
Precision-molded glass, acrylic, and eco-friendly PCR bottles designed for premium liquid supplements, cosmetic serums, and oral drops.
Get a Quote
Custom bioactive formulation blending Vitamin C micro-encapsulations with high-purity Niacinamide for nutricosmetic product lines.
Get a Quote
High-potency bulk active serum containing PDRN salmon DNA, targeted exosomes, and Centella Asiatica for institutional formulation brands.
Get a QuoteThe global sports nutrition and active lifestyle market demands uncompromised quality, ultra-pure protein fractions, and seamless regulatory compliance. Sourcing from the top whey protein suppliers requires rigorous analysis of raw dairy intake, processing technologies, and lot-to-lot consistency.
Modern B2B protein procurement goes far beyond matching price per kilogram. Enterprise buyers must evaluate Cross-Flow Microfiltration (CFM) purity profiles, heavy metal ICP-MS screening limits, instantization efficiency (sunflower vs. soy lecithin), and FDA 21 CFR Part 111 compliance. Selecting a contract manufacturing partner who owns the supply pipeline from raw whey isolate to finished packaged powder prevents multi-million dollar recall risks and label claim failures.
How top-tier sports nutrition brands assess prospective OEM contract facilities worldwide.
| Evaluation Vector | Industry Standard Requirement | Top Tier Tier-1 Manufacturer Standard | Brand Risk Mitigation Impact |
|---|---|---|---|
| Raw Material Origin | Sweet dairy whey byproduct derived from cheese yield. | rBST-free, grass-fed native dairy whey sourced directly from verified cooperative farms. | Prevents antibiotic residue compliance flags and improves natural amino acid retention. |
| Filtration Methodology | Ion-exchange chemical precipitation or thermal concentration. | Cold-processed Cross-Flow Microfiltration (CFM) & Ultrafiltration (UF). | Preserves native immunoglobulins (IgG), lactoferrin, and alpha-lactalbumin fractions without denaturing. |
| Heavy Metal & Contaminant Testing | Periodic composite batch testing for Cadmium, Lead, Arsenic, Mercury. | 100% Lot ICP-MS testing with analytical COAs provided per individual production run. | Guarantees compliance with California Proposition 65 and international import safety laws. |
| Instantization & Solubility | Standard mechanical ribbon blending with basic soy lecithination. | Non-GMO sunflower lecithin agglomeration via fluid-bed spray dryer. | Eliminates clumping, reduces foaming, and provides allergen-free allergen declarations. |
| Regulatory Audits | Standard state-level food facility licensing. | cGMP Certified (21 CFR Part 111), FDA Registered, Halal Certified, Kosher Certified. | Ensures smooth customs clearance across North America, EU, Middle East, and Asia-Pacific regions. |
The sports nutrition and functional food industry is undergoing a structural evolution driven by clean-label mandates, environmental transparency, and precision bioprocessing. Brand managers and global buyers must align with manufacturers capable of adapting to these key technological shifts.
Traditional whey protein is derived as a secondary byproduct of cheese production, exposing protein chains to enzymatic cheese-making starters and thermal pasteurization cycles. The industry is rapidly transitioning toward Native Whey Isolate (NWI), extracted directly from skim milk using low-temperature membrane filtration. Native whey yields up to 17% higher Leucine concentrations and intact immunoglobulins, creating premium positioning opportunities for high-end brands.
Consumer demand for rapid gastrointestinal absorption and zero-bloat post-workout nutrition has accelerated the adoption of Hydrolyzed Whey Protein Isolates (WPH). Using proprietary endo- and exo-protease enzymatic treatments, contract manufacturers achieve precise Degrees of Hydrolysis (DH-4 to DH-15). This breaks long peptide chains into di- and tri-peptides, dramatically reducing gut transit time and accelerating plasma amino acid spikes without impairing flavor.
Global regulatory bodies and environmental packaging mandates are pushing brands away from single-use HDPE rigid tubs. Leading suppliers are offering 100% recyclable mono-material pouches, post-consumer recycled (PCR) plastics, and carbon-neutral freight logistics. Procurement teams now prioritize suppliers with verifiable environmental, social, and governance (ESG) metrics and localized toll-blending facilities to minimize carbon transportation footprints.
The manufacturing gap between standard bulk commodity powder and elite sports nutrition formulas lies in technical bioprocessing. Here is how modern contract processing facilities maximize biological value and flavor stability.
Unlike legacy chemical ion-exchange isolation—which uses hydrochloric acid and sodium hydroxide to precipitate proteins while destroying delicate bio-fractions—modern CFM utilizes ceramic membranes with micro-pore diameters down to 0.1 microns. Operating under non-thermal, low-pressure conditions, CFM isolates pure whey proteins without denaturing immunoglobulins (IgG), lactoferrin, or bovine serum albumin (BSA), resulting in a 90%+ protein concentration with minimal fat, lactose, and cholesterol.
Native whey isolate powder naturally exhibits hydrophobic surface properties, leading to unwanted floating clumps when mixed in water. Manufacturers utilize multi-stage fluid-bed agglomerators to spray atomized non-GMO sunflower lecithin onto suspended protein particles. This process forms porous, rehydratable granules that dissolve completely in under 10 seconds of shaking without requiring high-shear electric blenders or synthetic anti-foaming chemicals.
Whey isolates and hydrolysates often carry natural dairy sourness or bitter peptide notes. Advanced contract formulators employ micro-encapsulated natural flavor systems, clean sweetening matrices (sucralose, purified stevia Rebaudioside-M, monk fruit), and high-capacity stainless steel ribbon blenders with double-helical agitators. This guarantees homogenous active ingredient dispersion across multi-ton production batches down to a 99.8% uniformity standard.
Partnering with a world-class USA contract manufacturer provides your brand with the stability, speed, and regulatory protection required to dominate competitive international markets.
All protein formulation, powder blending, tub filling, and pouch sealing take place inside our state-of-the-art facility in Norcross, Georgia, USA. Operating strictly under FDA 21 CFR Part 111 dietary supplement regulations, our facility maintains climate-controlled cleanrooms, HEPA air filtration, and continuous environmental microbial sampling to prevent cross-contamination.
From incoming raw whey drum inspection to final pallet shrink-wrapping, every single ingredient is tied to an internal batch record, supplier Certificate of Analysis (COA), and lot tracking code. Our in-house quality assurance team verifies raw material identity using Fourier Transform Infrared Spectroscopy (FTIR) and conducts heavy metal, micro, and potency testing prior to batch release.
We eliminate friction for emerging and enterprise brands alike. Enjoy flexible minimum order quantities starting as low as 500 tubs for custom powder blends or 1,000 units for private label catalogue products. Our in-house graphic team verifies Supplement Facts regulatory panels, while our packaging line handles shrink banding, scoops, induction seals, and export cartoning.
Essential technical, operational, and commercial answers for brand owners, purchasing directors, and global importers.
Connect directly with our senior formulation specialists and contract account directors in Norcross, GA. Get detailed batch pricing, custom flavor samples, and lead-time schedules tailored to your project goals.