In the contemporary fast-moving consumer goods (FMCG), personal care, and dietary supplement sectors, Formula Research & Development (R&D) serves as the central engine of brand differentiation and regulatory compliance. The market shift away from generic white-label stock formulations toward target-specific, bio-available, and clinically validated active ingredients has transformed how global brand owners evaluate contract manufacturers and chemical sourcing partners. Today’s procurement executives no longer look solely for high-volume mixing plants; they require strategic innovation hubs capable of multi-phase raw material characterization, scale-up stability testing, and complete global dossier compilation.
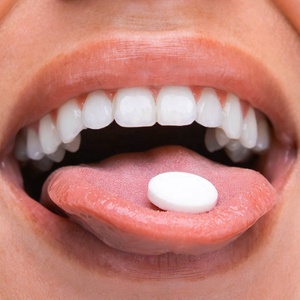
Navigating the global landscape of contract suppliers requires evaluating advanced technical parameters: reverse engineering capability, green chemistry extraction, cellular bio-assay validation, and micro-encapsulation delivery systems. Whether developing active dermocosmetics utilizing Salmon DNA Exosomes and Niacinamide complexes, or formulating shelf-stable oral delivery tablets such as PAP+ eco-friendly toothpaste tablets, partnering with top-tier R&D facilities is the single most critical factor in mitigating supply chain risk, securing intellectual property, and accelerating time-to-market.
To establish rigorous benchmarks for global brand owners, our senior R&D and analytical team evaluated over 120 international manufacturing plants against key performance indicators (KPIs) including analytical equipment density, batch-to-batch consistency, FDA/cGMP compliance track records, and custom synthesis capabilities.
| R&D Evaluation Criteria | Tier 1 Premium R&D Laboratories | Standard Contract OEM Plants | Impact on Brand Commercialization |
|---|---|---|---|
| Analytical Infrastructure | HPLC-MS, GC-MS, FTIR, Rheometry, UV-Vis Spectrophotometry | Basic Viscometers, pH Meters, Standard Titration | Ensures precise active compound quantification & stability verification. |
| Formula Stability Testing | Accelerated (40°C/75% RH), Real-Time, Freeze-Thaw, Photostability | Basic temperature oven observation (3-month max) | Prevents phase separation, oxidation, and recall risks over shelf life. |
| Scale-Up Technology | Pilot-scale vacuum emulsifiers, ribbon blenders, fluid-bed dryers | Direct transfer from bench to large-scale kettles | Eliminates viscosity and particle-size discrepancies in commercial runs. |
| Regulatory & Quality Audits | cGMP, FDA Registered, ISO 22716, ISO 9001, Halal, Kosher | Basic local sanitation permits & basic manufacturing licenses | Guarantees friction-free customs clearance and global market access. |
| Intellectual Property (IP) | Exclusive proprietary formulation transfer, full custom IP ownership | Shared stock formulations with minimal customization | Protects brand equity and creates defensible market barriers. |
With more than two decades of dedicated trade expertise operating out of our state-of-the-art facility in Norcross, Georgia, USA, our integrated R&D and production infrastructure sets the standard for dietary supplement and cosmetics formulation contract manufacturing. By housing procurement, chemical formulation, regulatory engineering, artwork design, and fill-finish execution within a single unified facility, we eliminate the operational delays and miscommunications typical of fragmented supply chains.
Our in-house master chemists transform bio-active target profiles into stable, highly bioavailable capsules, powders, chewables, serums, and emulsions tailored to precise consumer claims.
Operating under strict U.S. FDA regulations and cGMP standards. Every production lot undergoes rigorous raw material identity verification and full batch-record documentation.
From initial raw material receipt through blending, encapsulation, and outer packaging, every batch is locked to verified Certificates of Analysis (COAs) for end-to-end transparency.
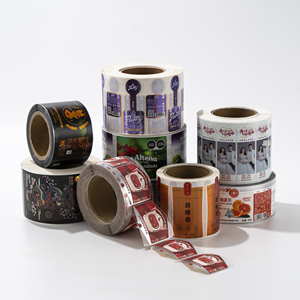
In-house structural designers build compliant Supplement Facts and Ingredient Declarations alongside high-barrier vinyl labeling, custom bottles, tubs, and eco-friendly pouches.
Equipped with complete documentation support including Certificates of Free Sale, Halal Certificates (upon request), and technical dossiers required for customs entry in 40+ countries.
Low minimum entry points (MOQs starting at 500–1,000 units for select private label formats) allow rapid market testing prior to scaling to multi-million unit high-speed runs.
As global supply chains navigate regulatory tightening and changing consumer values, procurement officers must align with suppliers capable of supporting next-generation formulation trends. Key shifts dominating contract manufacturing over the next five years include:
1. Bio-Fermented & Cellular Actives: Traditional botanical extracts are rapidly giving way to biotechnology-derived active ingredients. The integration of Exosomes, Centella Tox complexes, and bio-fermented Salmon DNA represents a quantum leap in skin-barrier cellular repair and collagen synthesis support, requiring specialized cold-process emulsion facilities.
2. Waterless & Concentrated Formulations: Environmental directives are driving demand for solid, anhydrous, and dry-format consumer products. Innovation in formats like PAP+ Toothpaste Tablets reduces shipping weight, eliminates plastic tube waste, and extends formula shelf life without harsh chemical preservatives.
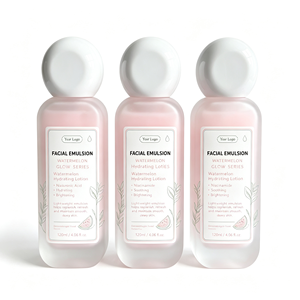
3. Clean-Label Synergy & Multi-Active Complexes: Consumers expect multi-benefit efficacy in single products. Modern R&D targets synergistic bioactive pairings—such as pairing Watermelon Niacinamide with stabilized Vitamin C—demanding advanced buffering systems to maintain active potent storage stability without discoloration or degradation.
4. Sustainable Packaging Compliance: Procurement teams must evaluate primary and secondary packaging in tandem with formulation chemistry. High-performance adhesive vinyl sticker rolls and barrier packaging must withstand oil migration, alcohol solvents, and moisture without compromising eco-recyclability standards.
Achieving commercial success requires bridging active ingredient selection with precise processing mechanics. Below is an analytical breakdown of prominent product categories manufactured across top-tier contract facilities:
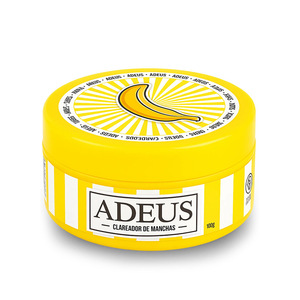
A. Advanced Anti-Hyperpigmentation Emulsions (Banana Anti Dark Spot Cream)
Formulating targeted hyperpigmentation correctors requires stabilized botanical lipophilic extracts combined with potent tyrosinase inhibitors. Key technical challenges involve preventing photo-oxidation of organic active compounds while maintaining an elegant, non-comedogenic skin feel across varying lipid concentrations.
B. High-Potency Exosome & Peptide Serums (Korean-Style Exosome Salmon DNA Complex)
Facial serums utilizing Exosome vesicle delivery mechanisms require precise temperature control during high-shear mixing. Micro-emulsification technology ensures nano-sized lipid carriers remain suspended without agglomeration, allowing deep cellular penetration and optimal stability for delicate active bio-molecules.
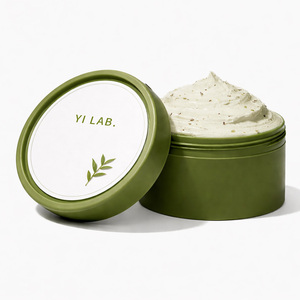
C. Sheet Mask Bio-Cellulose Saturations (Green Tea Mud & Rose Sheet Masks)
Impregnating non-woven fabrics or bio-cellulose matrices with organic deep-cleansing serums demands strict microbiological controls. Formulations incorporating green tea polyphenols and natural clays require controlled viscosity profiles to ensure uniform serum distribution without sediment settling during continuous packaging operations.
Answers to crucial commercial, technical, and regulatory questions when engaging a contract R&D factory:
Connect with our expert R&D formulators and project managers to evaluate your active ingredient specifications, request bench samples, and receive a complete turnkey manufacturing proposal.
Get a Quote