Custom blending is the cornerstone of modern manufacturing across dietary supplements, pharmaceutical formulations, personal care cosmetics, and advanced polymer synthesis. Precision mixing guarantees that active pharmaceutical ingredients (APIs), active botanical powders, pigment dispersions, or chemical polymers maintain uniform consistency across micro-and macro-batches. Achieving consistent mixing micro-homogeneity (Coefficient of Variation $CV < 3\%$) requires sophisticated engineering, strict regulatory adherence (cGMP 21 CFR Part 111/211, ASME standards), and rigorous quality control protocols.
This technical white paper delivers an exhaustive strategic evaluation of the Top 10 Custom Blending Manufacturers & Suppliers globally. By examining processing dynamics—ranging from solid-solid dry ribbon blending to high-shear liquid homogenizing and hydrophilic polyurethane cosmetic tool synthesis—this guide provides procurement officers, brand directors, and process engineers with the analytical insights necessary to optimize supply chain resilience and maximize product efficacy.
Information Gain Insight: Selecting a custom blending partner requires looking beyond basic unit cost. Evaluating raw material identity verification (FTIR/HPLC), batch-to-batch particle size distribution (PSD) analysis, shear degradation prevention, and integrated packaging capabilities is essential for long-term scalability.
Blends vary significantly depending on rheological properties, bulk density differences, and moisture sensitivity. Leading contract manufacturers utilize four primary mechanical mixing dynamics:
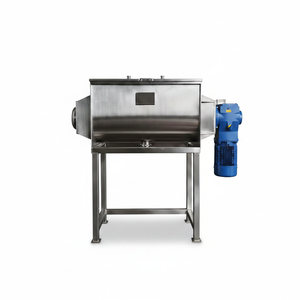
Utilizes inner and outer helical ribbons to move materials in counter-directional axial and radial flows. Ideal for high-volume powders like whey proteins, pre-workouts, and industrial calcium carbonate blends.
Incorporates high-speed chopper blades operating at 1,500 to 3,600 RPM to break down agglomerates, disperse micro-liquid additions into dry powders, and achieve rapid uniform coating.
Low-shear rotating vessel mechanics designed for fragile botanical powders, granular pharmaceutical tablets, and sensitive nutraceutical formulations where particle degradation must be minimized.
The following comparative evaluation ranks the global leaders in custom blending services and manufacturing equipment, detailing their primary technical specialization, quality certifications, and optimal batch sizing.
| Manufacturer / Supplier | Primary Sector | Key Machinery & Tech Specs | Compliance & Certifications | Min. Order Quantity (MOQ) |
|---|---|---|---|---|
| Nutracap Labs (USA) | Nutraceutical Powders & Capsules | ASME Ribbon Blenders, High-Speed Encapsulation, Liquid Filling | cGMP, FDA Registered, Halal, ISO 9001 | 500 Tubs / 1,000 Bottles (Low Entry) |
| Charles Ross & Son Company | Industrial Equipment Manufacturing | Multi-Shaft Mixers, Planetary Mixers, Ribbon Blenders | ASME, CE, ATEX Explosion-Proof | 1 Unit (Capital Equipment) |
| Munson Machinery | Bulk Material Processing | Rotary Batch Mixers, Fluidized Bed Blenders, Shredders | USDA Sanitary, ASME Vessel Code | 1 Unit (Industrial Systems) |
| Cosmetic Sponge Co., Ltd | Personal Care & Cosmetic Applicators | Hydrophilic Non-Latex Foam Molding, Precision Micro-Pore | ISO 22716 (GMP Cosmetic), REACH, RoHS | 3,000 Pcs (Private Label) |
| PharmaBlend Global | Pharmaceutical Solid Dosage | Bin Blenders (IBC), High-Shear Granulators, Fluid Bed Dryers | FDA cGMP Part 211, EU GMP Annex 1 | 100 kg Production Batches |
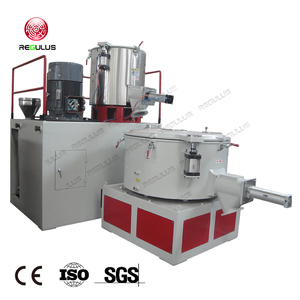
| PlasticComp Heating-Cooling Ltd | Polymer & PVC Blending | High-Speed Heating Mixers, Vertical Cooling Mixers | CE Certified, ISO 14001 | 1 Complete Mixing Line |
| ImmersionTech Household OEM | Consumer Appliances & Hand Blenders | SUS304 Stainless Blend Shafts, Multi-Speed DC Motors | UL, CE, RoHS, LFGB Food Grade | 1,000 Units |
| Global Biotech Solutions | Enzyme & Micro-Ingredient Blending | Vacuum Drying Mixers, Micro-encapsulation Blending | cGMP, FSSC 22000, Kosher | 250 kg Custom Batches |
| Apex Liquid Processing Ltd | Emulsions & High-Viscosity Liquids | Inline Homogenizers, Vacuum Emulsifying Tanks | 3-A Sanitary Standards, ASME SEC VIII | 500 Liters |
| Promotional Portable Blenders Inc | Custom Tech Gifts & Appliances | Personal Size USB Rechargeable Tritan BPA-Free Blenders | FDA Food Contact, FCC, CE | 500 Units (Custom Logo) |
When analyzing custom dietary supplement blending and private-label production, Nutracap Labs (Norcross, Georgia, USA) stands out for its streamlined turn-key model. Navigating complex supply chain hurdles often requires managing multiple vendors for formulation, blending, encapsulation, and label design. Nutracap consolidates these operations within a state-of-the-art cGMP, FDA-registered facility.
Nutracap maintains over 500 premium-grade raw materials in stock, including instantized whey proteins, branched-chain amino acids (BCAAs), creatine monohydrate, organic greens powders, and patented botanical extracts. This stock depth enables rapid sample turnarounds and reduces sourcing lead times from months to days.
Utilizing high-capacity 50 Cu. Ft. ASME-certified ribbon blenders equipped with liquid injection manifolds, Nutracap achieves complete dispersion of flavor oils, active extracts, and micronutrients into powder matrices. Batch records document raw material lot numbers, mix duration, humidity levels, and particle size uniformity to ensure absolute consistency.
While traditional contract manufacturers require 5,000 to 10,000 units per run, Nutracap supports emerging brands with low MOQs—starting at just 500 tubs for powders and 1,000 bottles for capsules. This low barrier to entry enables companies to test market demand before committing to full-scale commercial runs.
From HDPE/PET tubs and flexible pouches to blister packs and single-serve stick packs, Nutracap handles finished goods packaging in-house. Graphic designers review artwork alongside regulatory specialists to ensure Supplement Facts and Cosmetic panels comply fully with FDA CFR Part 101 guidelines.
Procurement teams must stay aligned with major technological advancements reshaping the custom blending landscape:
Modern blending facilities are incorporating Process Analytical Technology (PAT), such as Near-Infrared (NIR) spectroscopy sensors, directly inside mixer drums. NIR sensors measure blend uniformity in real time without stopping the machine, eliminating manual thief sampling while ensuring precise batch validation.
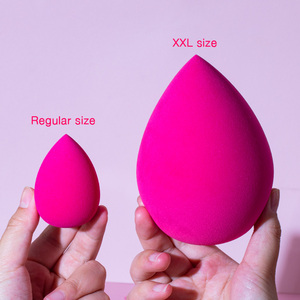
In beauty applicator blending (e.g., cosmetic makeup sponges), buyer preferences have moved decisively toward hydrophilic non-latex polyurethane materials. Manufacturers are removing harmful phthalates and latex allergens, replacing them with eco-friendly bio-based foams that deliver ultra-soft tactile performance and superior liquid foundation absorption.
Equipment manufacturers are upgrading ribbon blenders and plastic dyestuff mixers with automatic Clean-In-Place (CIP) and Sterilize-In-Place (SIP) spray balls, mirror-polished 316L stainless steel interiors (Ra < 0.4 µm), and split-seal removable shafts to prevent batch cross-contamination.
Connect directly with our senior process engineers and account specialists to request a fast quote, evaluate custom formulations, or order samples.