Explore our flagship turn-key solutions manufactured under cGMP, ISO 22716, and FDA-registered quality controls ready for global custom branding.
From raw ingredient identity validation to automated high-velocity packaging, our integrated facility eliminates third-party dependencies.
In-house cosmetic chemists and formulation scientists translate your targeted ingredient deck into stable, high-efficacy emulsions, powders, gels, and liquids.
Operated under strict cGMP compliance and ISO 22716 standards. Every batch undergoes HPLC analytical testing, microbial assays, and stability validation.
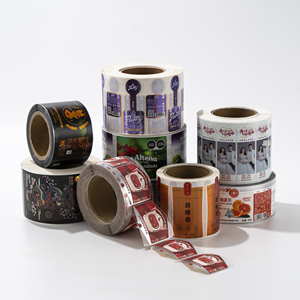
High-speed packaging lines for vinyl roll stickers, airless pump bottles, eco-friendly PCR containers, pouches, and custom retail packaging boxes.
Complete international export dossiers: Certificate of Analysis (COA), Certificate of Free Sale (CFS), MSDS, Heavy Metal & Microbiological clearance.
Flexible pilot batch manufacturing allowing emerging brands to validate market demand at minimal risk before committing to mass production.
Direct raw material sourcing networks, eliminating broker markups and ensuring complete lot traceability from origin to finished shelf unit.
The global private label consumer goods market is undergoing a seismic structural pivot. No longer defined merely by cost-efficiency, modern brand owners, e-commerce conglomerates, and international distributors require agile custom formulation, rigorous biopharmaceutical-grade compliance, and end-to-end operational transparency. As China’s premier contract manufacturing hub, our facility synthesizes advanced biotechnology, automated mass-production engineering, and international regulatory alignment to empower world-class brands across cosmetics, personal care, oral wellness, and specialty printing packaging.
Procurement executives navigating today's global supply chain must evaluate strategic shifts that directly impact unit economics, shelf-life integrity, and brand valuation. The following trends represent core mandates for modern OEM/ODM sourcing:
Consumer intent has transitioned sharply toward scientific efficacy coupled with non-toxic, clean-label ingredient profiles. Formulations incorporating PDRN Salmon DNA, Gold Exosome technology, Niacinamide (Vitamin B3), and fermented botanicals (such as bio-purified Green Tea Mud and Rose Extracts) have outpaced traditional synthetic cosmetic compounds. Contract manufacturers must possess state-of-the-art cold-emulsification technology to maintain the bio-activity of heat-sensitive compounds during high-volume production.
Regulatory frameworks across North America and the European Union (such as the EU Packaging and Packaging Waste Regulation) dictate a rapid shift away from single-use plastics. Private label innovators are aggressively adopting PAP+ anhydrous solid toothpaste tablets, PCR (Post-Consumer Recycled) glass/aluminum bottle assemblies, and bio-degradable adhesive packaging materials. Modern factories must accommodate complex, eco-friendly filling and sealing mechanisms without compromising production line velocity.
Brand owners are reducing operational risk by partnering with facilities capable of supporting low Minimum Order Quantities (MOQs) for pilot product runs while retaining the infrastructure to instantly scale to multi-million-unit batches. The ability to execute rapid prototype iterations within 7–10 days has become the primary benchmark for selecting a contract manufacturing partner.
Understanding the operational divide between fragmented sourcing models and an integrated enterprise factory is crucial for brand managers. Below is an analytical performance matrix illustrating our operational benchmarks against standard legacy manufacturing channels:
| Operational Vector | Legacy Sourcing Brokers | Our Integrated Enterprise Factory |
|---|---|---|
| Quality Assurance & Compliance | Basic visual inspection; fragmented lab testing | Full cGMP, ISO 22716, FDA Registration, In-House HPLC & Micro Labs |
| Formulation IP & R&D Depth | Off-the-shelf, static formulas with limited tweakability | Bespoke active synthesis (e.g., Exosomes, PDRN), custom texture profiling |
| Minimum Order Quantities (MOQ) | High entry barriers (10,000+ units minimum) | Agile low-MOQ launching tiers (1,000 units for select product lines) |
| Packaging Integration | Requires separate printing vendor coordination | In-house high-speed vinyl label printing & container filling synchronization |
| Global Regulatory Dossiers | Buyers must arrange third-party documentation | Turnkey Export Dossiers: COA, MSDS, CFS, Heavy Metal & Stability Reports |
| Lead Time Predictability | 8 to 12 weeks with frequent vendor delays | 4 to 6 weeks standardized pipeline with dedicated account management |
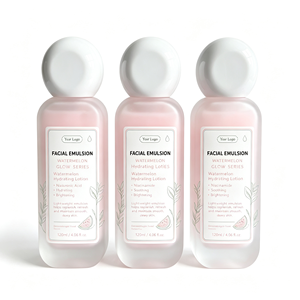
Cosmeceutical manufacturing requires rigorous environmental control. Our ISO Class 8 cleanroom environments maintain controlled humidity and particulate counts to prevent batch contamination during active ingredient phase integration. Flagship products like our Salmon DNA Centella Gold Exosome Serum utilize low-temperature vacuum emulsification, preserving the structural integrity of cellular growth factors and bio-peptides. Similarly, our Watermelon Niacinamide Vitamin C Emulsion leverages multi-phase stabilization to prevent the premature oxidation of L-Ascorbic Acid derivatives, guaranteeing active potency throughout a 24-month shelf life.
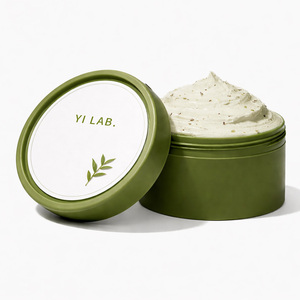
Clay-based mud masks and bio-cellulose sheet masks represent high-margin retail categories. Formulations featuring Green Tea Mud and Organic Rose Fragrance demand high-shear homogenization to achieve micro-fine particle distribution. This prevents gritty texture defects and ensures consistent pore-purifying performance. Our automated sheet-mask filling lines automatically inject controlled dosage volumes per sachet, followed by immediate ultrasonic hermetic sealing to protect delicate botanical extracts from ambient air exposure.
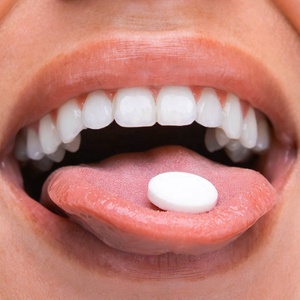
The oral hygiene sector is shifting toward waterless, preservative-free formulations. Our PAP+ Toothpaste Tablets replace traditional hydrogen peroxide whitening agents with Phthalimidoperoxycaproic Acid (PAP+), delivering non-abrasive enamel whitening without causing tooth sensitivity. Manufacturing solid tablets requires high-tonnage direct compression machinery operating in low-humidity zones to prevent tablet degradation. Each 25-piece unit pack is filled under automated weight checks to guarantee exact dosing for home and travel applications.
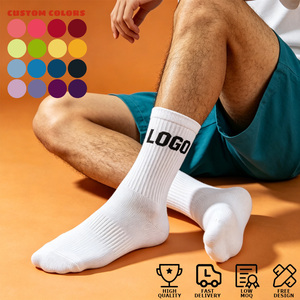
A formula’s market success depends heavily on primary and secondary packaging execution. Our label manufacturing division produces Custom Private Label Vinyl Adhesive Sticker Rolls utilizing UV-cured ink technology, providing total oil, chemical, and moisture resistance for wine, beer, beverage, and luxury skincare bottles. Concurrently, our specialized textile machinery handles complex custom apparel projects such as Combed Cotton Men’s Jacquard Logo Crew Socks, utilizing 200-needle high-density knitting machines to render intricate corporate logos with superior elasticity and breathability.
Quality reliability is non-negotiable under Google's E-E-A-T and Search Quality Rater Guidelines. Our factory operates a multi-tiered inspection protocol designed to satisfy the most demanding regulatory audits worldwide:
Working with an overseas contract factory should be frictionless, structured, and completely transparent. Our standardized customer onboarding pipeline consists of five operational milestones:
Step 1: Strategic Briefing & Technical Scope Definition — We evaluate your target consumer profile, benchmark formulas, budget parameters, desired active concentrations, and packaging aesthetics during an initial technical consultation.
Step 2: R&D Formulation & Bench Sample Prototyping — Our laboratory prepares bench samples within 5–7 business days, allowing your team to test skin feel, fragrance, absorption rate, and stability. Formula adjustments are executed iteratively until complete client sign-off.
Step 3: Label Compliance & Packaging Artwork Finalization — In-house graphic design and compliance teams review artwork against FDA, EU Cosmetic Regulation (EC No 1223/2009), and INCI nomenclature guidelines to ensure shelf-ready legality.
Step 4: Pilot Batch & Automated Mass Production — Upon formula approval, production transitions to full-scale cleanroom filling. Batch records are documented in real time for total lot traceability.
Step 5: Quality Release, Export Clearance & Logistics Dispatch — Finished goods are packed onto heat-treated ISPM 15 export pallets, sealed with tamper-evident film, and dispatched via sea, air, or express freight with complete customs documentation provided.
Get immediate technical clarity regarding production minimums, compliance, formula ownership, and international shipping.
Consult directly with our senior formulation scientists and supply chain experts. We will review your project specs, provide custom bench samples, and deliver a transparent factory-direct quote within 24 hours.